standard-title
SVP Injections, Ampoules, Vials, and Dry Powder Taj Pharma’s Kalgam facility leads in SVP injections, ampoules, vials, and dry powders, integrating advanced technology, strict quality control, and sustainable practices to deliver high-quality pharmaceuticals globally.
SVP Injections, Ampoules, Vials, and Dry Powder
Taj Pharma’s Kalgam facility leads in SVP injections, ampoules, vials, and dry powders, integrating advanced technology, strict quality control, and sustainable practices to deliver high-quality pharmaceuticals globally.
Taj Pharma stands as a global leader in the pharmaceutical industry, driven by its unwavering commitment to innovation, quality, and excellence. Our Manufacturing Plant II, located in the serene yet strategically significant Kalgam Village, Valsad, Gujarat, is a cornerstone of our sterile injectable product line. From Small Volume Parenterals (SVP) to ampoules, vials, and dry powder formulations, the plant exemplifies world-class manufacturing standards. This article delves into the unparalleled infrastructure, advanced technology, and rigorous processes that have solidified Taj Pharma’s reputation on the global stage.
Small Volume Parenterals (SVP) Injections: Precision in Every Dose
At Taj Pharma, we understand the critical importance of Small Volume Parenterals (SVP) in modern healthcare. These injectable solutions are meticulously crafted to deliver precise therapeutic effects while adhering to global safety standards. Our Kalgam plant is equipped to produce over 10 million units of SVP injections monthly, meeting the needs of patients and healthcare providers worldwide.
Key Features of SVP Production
High-Quality Raw Materials: Pharmaceutical-grade solvents and Active Pharmaceutical Ingredients (APIs) sourced from trusted global suppliers.
Diverse Applications: SVP formulations for antibiotics, analgesics, vaccines, and specialized treatments.
Superior Packaging: Tamper-evident ampoules and vials to ensure product integrity and safety during transport.
Our commitment to precision ensures every batch is contamination-free and retains maximum therapeutic efficacy, meeting stringent regulatory requirements from markets such as the US, EU, and WHO-compliant regions.
Ampoule Manufacturing: Redefining Quality and Safety
Ampoules are the preferred choice for single-dose injectable solutions due to their hermetically sealed, contamination-resistant design. At Taj Pharma, we have revolutionized ampoule production with state-of-the-art technology and rigorous quality controls.
Advanced Ampoule Production Processes
Type I Borosilicate Glass: Used for its exceptional resistance to thermal shock and chemical reactions.
Automated Cleaning: Multi-stage ampoule washing using purified water and Water for Injection (WFI).
Precision Filling: Volumetric filling machines guarantee an accuracy level of ±1%, ensuring each ampoule contains the precise dosage.
Our ampoules are available in 1ml, 2ml, 5ml, and 10ml sizes, catering to a variety of therapeutic applications, including vaccines, anesthesia, and specialized medications.
Vial Production: Versatility and Compliance
Our vial production capabilities stand out for their versatility and global reach. From liquid formulations to lyophilized powders, the Kalgam plant is equipped to deliver excellence across all vial-based products.
Key Advantages of Taj Pharma’s Vial Line
Customization: Options for clear and amber glass vials ranging from 2ml to 100ml, designed to protect the product from light and contamination.
Ready-to-Use Vials: Pre-sterilized vials with elastomeric closures for convenience and safety.
Regulatory Compliance: Manufactured under EU-GMP guidelines, our vials meet the standards of regulatory bodies in Europe, Africa, and the Americas.
Enhanced Features: Tamper-proof caps, colored flip-offs, and comprehensive labeling solutions tailored to client requirements.
Dry Powder Manufacturing: Stability and Longevity
Lyophilized dry powders are critical for sensitive biologics and antibiotics, offering extended shelf life and stability. Taj Pharma’s dry powder manufacturing division sets a benchmark in freeze-drying technology.
Highlights of the Dry Powder Division
Lyophilizers with Advanced Capabilities: Our 20-square-meter freeze-drying chambers operate at temperatures as low as -50°C, preserving the integrity of thermolabile compounds.
Wide-Ranging Expertise: Specialization in formulating proteins, peptides, and other sensitive molecules.
Dual-Chamber Packaging: Designed for easy reconstitution at the point of care, enhancing patient convenience and safety.
Stringent Quality Checks: Residual moisture analysis and sterility testing ensure the highest safety and efficacy standards.
Uncompromising Quality Assurance
Taj Pharma’s dedication to quality surpasses compliance. Our Quality Control (QC) and Quality Assurance (QA) teams implement multi-layered processes to ensure products meet and exceed regulatory expectations.
Our Quality Framework
Raw Material Testing: Comprehensive screening of solvents and APIs for pharmacopeial compliance.
In-Process Monitoring: Real-time checks for pH levels, particulate matter, and fill volumes.
Final Product Validation: Stringent sterility, endotoxin, and stability testing in adherence to ICH guidelines.
The Kalgam plant holds prestigious certifications, including WHO-GMP, ISO 9001, and ISO 14001, showcasing our commitment to sustainable and ethical practices.
State-of-the-Art Infrastructure
Spanning 15 acres, the Kalgam facility integrates cutting-edge technology to ensure efficiency, precision, and scalability.
Key Infrastructure Highlights
BFS (Blow-Fill-Seal) Technology: Enables the production of sterile liquid doses in flexible containers.
Isolator Systems: Maintain a Grade A environment for aseptic processing, ensuring product sterility.
SCADA Systems: Real-time monitoring of manufacturing parameters to guarantee consistent quality.
Adjacent to the manufacturing unit, our Research and Development (R&D) center drives innovation in formulation and process optimization, enabling us to meet the evolving needs of global healthcare.
Sustainability: Pioneering Green Manufacturing
At Taj Pharma, sustainability is a core value. We have integrated eco-friendly practices across all operations at the Kalgam plant.
Sustainable Initiatives
Zero Liquid Discharge (ZLD): Advanced water recycling systems ensure no wastewater leaves the facility.
Solar Power Utilization: On-site solar panels fulfill 30% of our energy requirements.
Waste Management: Biohazardous waste is safely incinerated at temperatures exceeding 1200°C.
Strategic Location for Global Reach
The Kalgam plant’s strategic location on the Coastal Highway Road in Valsad ensures seamless connectivity for domestic and international distribution.
Logistical Advantages
Proximity to Ports: Situated just 150 km from Mundra Port, facilitating efficient exports.
Skilled Workforce: Strong collaboration with local technical institutes ensures access to a highly skilled workforce.
Global Supply Chain: Robust partnerships with leading API suppliers ensure uninterrupted production.
Our Commitment to Global Health
Taj Pharma’s Kalgam facility embodies our mission to provide affordable, high-quality pharmaceuticals that save lives. By combining advanced technology, rigorous quality standards, and sustainable practices, we contribute to the global healthcare landscape with integrity and excellence.
Mefloquine Hydrochloride Tablets 250mg Manufacturer in India | Taj Pharma – Global Supplier & Exporter Mefloquine Hydrochloride Tablets 250mg Manufacturer, Supplier and Exporter from India Taj Pharma is an established Mefloquine Hydrochloride Tablets 250mg manufacturer in India, supplying high-quality pharmaceutical formulations to regulated and emerging international markets. Manufactured at our facility in Vapi, Gujarat, India, our Mefloquine Hydrochloride Tablets 250mg (Mexoquin) are produced using carefully controlled manufacturing processes, quality-tested raw materials, and comprehensive quality assurance systems. We serve pharmaceutical importers, distributors, institutional buyers, government procurement agencies, hospitals, wholesalers, and private-label partners across Africa, the Middle East, Latin America (LATAM), Asia, and other international markets. Mefloquine Hydrochloride Tablets About Mefloquine Hydrochloride Tablets 250mg Mefloquine Hydrochloride Tablets 250mg is a prescription antimalarial medicine used for the prevention and treatment of malaria in accordance with approved prescribing information and local clinical guidelines. It should always be used under the supervision of a qualified healthcare professional. Mefloquine acts against malaria parasites and is prescribed for specific indications based on medical assessment, travel requirements, and regional resistance patterns. Trusted Pharmaceutical Manufacturing by Taj Pharma Our manufacturing operations are built around product quality, consistency, and regulatory compliance. Our manufacturing capabilities include: Modern production facilities Validated manufacturing […]
Doxepin Hydrochloride Capsules 25mg Manufacturer, Supplier & Exporter in India – Taj Pharma Leading Doxepin Hydrochloride Capsules 25mg Manufacturer in India We are Taj Pharma, a trusted Doxepin Hydrochloride Capsules 25mg manufacturer, supplier, exporter, and PCD Pharma Franchise company in India, committed to providing premium-quality pharmaceutical products manufactured in accordance with international quality standards. Our (Doxphoria )Doxepin Hydrochloride Capsules 25mg are produced in advanced WHO-GMP compliant manufacturing facilities located in Vapi, Gujarat, ensuring consistent quality, safety, and reliability for healthcare providers and pharmaceutical businesses worldwide. With years of pharmaceutical manufacturing expertise, we supply Doxepin Hydrochloride Capsules 25mg across PAN India while exporting to Africa, the Middle East, Latin America (LATAM), Asia, and other international markets. We also provide comprehensive third-party manufacturing, contract manufacturing, private labeling, and PCD Pharma Franchise solutions to pharmaceutical companies looking for a dependable manufacturing partner. About Doxepin Hydrochloride Capsules 25mg Doxepin Hydrochloride Capsules I.P. 25mg Doxepin Hydrochloride Capsules 25mg belong to the tricyclic antidepressant (TCA) class of medicines. Under the supervision of a qualified healthcare professional, they are prescribed for the treatment of major depressive disorder and anxiety disorders. Depending on clinical evaluation and approved prescribing information, Doxepin may also be prescribed in selected patients for […]
Sodium Valproate Tablets 200mg Manufacturer in India Sodium Valproate Tablets 200mg: High-Quality Manufacturing and Global Supply from India Sodium Valproate Tablets 200mg are widely prescribed for the management of epilepsy, seizure disorders, bipolar disorder, mania, migraine prevention, and certain neurological conditions. As a trusted pharmaceutical manufacturer and exporter in India, we are committed to delivering premium-quality Sodium Valproate Tablets 200mg that comply with international pharmaceutical standards, ensuring safety, efficacy, and consistency in every batch. Our manufacturing operations are supported by advanced production facilities, stringent quality control systems, and highly experienced pharmaceutical professionals. We supply Sodium Valproate Tablets 200mg to healthcare institutions, distributors, pharmaceutical importers, government agencies, and PCD pharma franchise partners across India, Africa, the Middle East, Latin America, and various international markets. What Are Sodium Valproate Tablets 200mg? sodium valproate gastro resistant tablets 200mg Sodium Valproate is an anticonvulsant and mood-stabilizing medication used to control abnormal electrical activity in the brain. It helps reduce the frequency and severity of seizures and is commonly prescribed for neurological and psychiatric conditions. Sodium Valproate Tablets 200mg are primarily indicated for: Epilepsy Generalized seizures Partial seizures Bipolar disorder Acute mania Migraine prevention Trigeminal neuralgia Neurological disorders requiring anticonvulsant therapy The medication works by […]
Pantoprazole Sodium 40mg and Domperidone 30mg Capsules Manufacturer in India The demand for effective gastrointestinal medicines continues to grow across domestic and international pharmaceutical markets. We proudly stand among the leading Pantoprazole Sodium 40mg and Domperidone 30mg capsules manufacturers in India, delivering premium-quality formulations to healthcare companies, distributors, hospitals, government institutions, and international importers. At Taj Pharma India, we manufacture high-quality Pantoprazole Sodium Gastro Resistant 40mg and Domperidone Prolonged Release 30mg Capsules, marketed under the trusted brand name PANTAJ. Our advanced manufacturing facility located in Vapi, Gujarat, India follows stringent international quality standards to ensure safety, effectiveness, and consistency in every batch. We serve clients across Africa, Middle East, Latin America (LATAM), Asia, CIS countries, and emerging pharmaceutical markets worldwide, offering reliable manufacturing, third-party production, private labeling, and global export services. Leading Pantoprazole Sodium and Domperidone Capsules Manufacturer in India Pantoprazole Sodium 40mg and Domperidone 30mg capsules We are recognized as a reliable pharmaceutical manufacturer specializing in gastrointestinal formulations. Our expertise in producing Pantoprazole 40mg + Domperidone 30mg capsules allows us to serve both domestic and international pharmaceutical businesses efficiently. Our manufacturing unit is equipped with: Advanced capsule filling machinery High-capacity production lines Modern packaging systems In-house quality testing laboratories […]
Rabeprazole 40mg + Domperidone 30mg Capsules Manufacturer Supplier in India Rabeprazole 40mg + Domperidone 30mg Capsules Manufacturer in India We are a leading Rabeprazole 40mg + Domperidone 30mg Capsules manufacturer in India, delivering premium-quality pharmaceutical formulations for domestic and international markets. Taj Pharma is recognized for producing reliable gastroenterology medicines with strict adherence to quality standards, advanced manufacturing systems, and global regulatory compliance. Our Rabeprazole + Domperidone Capsules (RABETAJ) are formulated to provide effective relief from acidity, acid reflux, indigestion, GERD, bloating, nausea, and delayed gastric emptying. With world-class production facilities and a customer-focused approach, we serve clients across Africa, the Middle East, LATAM, Asia, and PAN India. What is Rabeprazole 40mg + Domperidone 30mg Capsules? Rabeprazole 40mg + Domperidone 30mg Capsules (RABETAJ) Rabeprazole 40mg + Domperidone 30mg Capsules is a combination medicine widely prescribed for digestive disorders. It combines: Rabeprazole 40mg – A proton pump inhibitor (PPI) that reduces excess stomach acid production. Domperidone 30mg – A prokinetic agent that enhances stomach motility and helps food move smoothly through the digestive tract. This dual-action formula offers fast and long-lasting relief for patients suffering from gastric discomfort and reflux-related conditions. Uses of Rabeprazole + Domperidone Capsules Our capsules are used […]
Epalrestat Tablets 150mg Manufacturer in India Manufacturer of Epalrestat Tablets 150mg in India We at Taj Pharma are a well-established and trusted Epalrestat Tablets 150mg manufacturer in India, offering high-quality pharmaceutical formulations under strict GMP-WHO certified standards. Our branded formulation Epalrestat Tablets 150mg (EPATAJ) is developed with precision to ensure maximum therapeutic efficacy, safety, and global compliance. As a reputed pharmaceutical company based in Vapi, Gujarat, India, we specialize in manufacturing, exporting, and supplying Epalrestat Tablets to regulated and semi-regulated markets including Africa, Middle East, and Latin America (LATAM). Our commitment to innovation and quality makes us a preferred partner for global healthcare distributors. What is Epalrestat 150mg (EPATAJ)? Epalrestat Tablets 150mg (EPATAJ) Epalrestat Tablets 150mg Sustained Release (EPATAJ) is an advanced aldose reductase inhibitor used primarily in the management of diabetic peripheral neuropathy, a common complication of long-standing diabetes. Diabetic neuropathy occurs due to prolonged elevated blood glucose levels, which leads to sorbitol accumulation in nerve cells. This causes nerve damage, resulting in symptoms such as: Tingling sensations in hands and feet Burning pain Numbness Loss of sensation Weakness in extremities Epalrestat works by inhibiting the enzyme aldose reductase, thereby preventing the accumulation of sorbitol and helping improve nerve […]
Perindopril Arginine 5mg + Indapamide 1.25mg Tablets Manufacturer in India Introduction to Perindopril Arginine + Indapamide Tablets (Cardixam) We are a globally recognized manufacturer, exporter, and supplier of Perindopril Arginine 5mg + Indapamide 1.25mg Tablets, marketed under the brand name Cardixam, delivering premium-quality antihypertensive formulations to international healthcare markets. This fixed-dose combination is widely prescribed for the effective management of hypertension (high blood pressure) and for reducing the long-term risk of cardiovascular complications such as heart attack and stroke. Our pharmaceutical formulation combines two clinically proven active ingredients—Perindopril Arginine (ACE inhibitor) and Indapamide (thiazide-like diuretic)—to provide dual-action blood pressure control with enhanced therapeutic efficiency and patient compliance. Composition and Mechanism of Action Perindopril Arginine 5mg + Indapamide 1.25mg Tablets (Cardixam) Perindopril Arginine 5mg Perindopril is an angiotensin-converting enzyme (ACE) inhibitor that works by relaxing and widening blood vessels. This reduces vascular resistance, allowing smoother blood flow and lowering blood pressure effectively. Indapamide 1.25mg Indapamide is a diuretic that helps the body eliminate excess sodium and water through urine. This reduction in fluid volume further contributes to lowering blood pressure and reducing strain on the cardiovascular system. Synergistic Dual Action The combination of Perindopril and Indapamide provides a synergistic effect: Improves […]
Orlistat Capsules 60mg Manufacturer Supplier in India Orlistat Capsules 60mg Manufacturer in India We are recognized as a reliable Orlistat Capsules 60mg manufacturer in India, delivering premium pharmaceutical formulations that meet domestic and international quality requirements. Our manufacturing expertise, strict quality systems, and advanced production facilities enable us to supply high-standard Orlistat Capsules to healthcare distributors, importers, hospitals, pharmacies, and government institutions worldwide. Orlistat Capsules 60mg is widely used for weight management, obesity treatment, and calorie-controlled therapy support. We manufacture this product under stringent GMP-compliant conditions to ensure purity, consistency, and effectiveness in every batch. India has become a preferred destination for pharmaceutical sourcing, and we stand among the trusted names for dependable Orlistat manufacturing and export services. What is Orlistat Capsules 60mg? Orlistat Capsules 60mg (Fetrasil) Orlistat Capsules 60mg is a clinically trusted medicine used to support weight reduction in overweight and obese adults. It works by reducing the absorption of dietary fat in the stomach and small intestine. The medicine blocks enzymes known as lipases, which are responsible for breaking down fats consumed in meals. When used together with a reduced-calorie diet and regular physical activity, Orlistat helps individuals achieve effective weight management goals. Our Orlistat Capsules 60mg […]
Pancreatin 212.5mg Tablets Manufacturer Supplier in India Pancreatin 212.5mg Tablets Manufacturer in India We are a trusted Pancreatin 212.5mg Tablets manufacturer in India, delivering premium-quality digestive enzyme supplements for domestic and international healthcare markets. Our manufacturing standards focus on purity, consistency, therapeutic effectiveness, and global regulatory compliance. As a reputed pharmaceutical exporter, we supply Pancreatin tablets to Africa, the Middle East, LATAM, Asia, and other international destinations with reliable logistics and documentation support. Pancreatin 212.5mg Tablets are widely used as pancreatic enzyme replacement therapy for patients requiring support in digestion. These tablets contain a combination of digestive enzymes such as amylase, lipase, and protease, which help break down carbohydrates, fats, and proteins for improved nutrient absorption. What is Pancreatin 212.5mg Tablets? Pancreatin BP 212.5mg Tablets Pancreatin 212.5mg Tablets are enteric-coated enzyme supplements formulated to withstand stomach acid and release active enzymes in the intestine. This targeted release mechanism ensures better absorption and higher efficacy. These tablets are commonly prescribed in conditions associated with reduced pancreatic enzyme secretion, including: Chronic pancreatitis Cystic fibrosis Pancreatic insufficiency Post-pancreatic surgery digestive support Malabsorption syndromes Indigestion due to enzyme deficiency Regular use under medical supervision may help improve digestion, reduce bloating, support nutrient utilization, and […]
Clozapine 100mg Tablets Manufacturer Supplier in India Clozapine 100mg Tablets Manufacturer in India We are a leading Clozapine 100mg Tablets manufacturer in India, delivering premium-quality pharmaceutical formulations for domestic and international markets. Our advanced manufacturing infrastructure in Vapi, Gujarat enables us to produce Clozapine tablets that comply with strict quality, safety, and regulatory standards. We supply to hospitals, distributors, pharmacies, healthcare institutions, and global importers seeking dependable psychiatric medicine manufacturers in India. Clozapine is a highly effective atypical antipsychotic medicine widely prescribed for treatment-resistant schizophrenia and for reducing suicidal behavior in patients with schizophrenia or schizoaffective disorders. We manufacture Clozapine 100mg tablets with precision to ensure consistent potency, purity, dissolution, and shelf stability. Top Clozapine 100mg Tablets Supplier from Vapi, Gujarat Clozapine 100mg Tablets (Baw) We have established ourselves as a trusted Clozapine 100mg Tablets supplier from Vapi, Gujarat, India, serving clients across PAN India and overseas markets. Our location in one of India’s major pharmaceutical hubs helps us ensure timely dispatch, efficient logistics, and uninterrupted supply. Our supply network covers: PAN India pharmaceutical distributors Government and private hospitals Psychiatry clinics and institutions Wholesalers and stockists International importers Contract manufacturing partners PCD pharma franchise associates We maintain ready stock and […]
Deflazacort 6mg Tablets Manufacturer Supplier in India Deflazacort 6mg Tablets Manufacturer in India We are a trusted Deflazacort 6mg Tablets manufacturer in India, delivering premium-quality pharmaceutical formulations that meet stringent international standards. Our manufacturing facilities are equipped with advanced technology, modern quality control systems, and certified production units to ensure every batch maintains consistency, safety, and therapeutic effectiveness. Deflazacort 6mg Tablets are widely prescribed for inflammatory and autoimmune conditions and are especially recognized for their role in managing Duchenne Muscular Dystrophy (DMD). We manufacture this medicine under strict GMP and WHO-compliant guidelines, ensuring high purity, accurate dosage, and dependable results for domestic and export markets. What is Deflazacort 6mg Tablets? Deflazacort 6mg Tablets (DMDTAJ) Deflazacort 6mg Tablets belong to the corticosteroid category of medicines. It works by reducing inflammation, suppressing immune reactions, and controlling swelling caused by various chronic medical conditions. This medicine is often prescribed in cases where long-term inflammation control is required. Doctors commonly recommend Deflazacort for: Duchenne Muscular Dystrophy Allergic disorders Asthma and respiratory inflammation Rheumatoid arthritis Skin disorders Autoimmune diseases Nephrotic syndrome Chronic inflammatory conditions Our tablets are formulated for excellent absorption and reliable patient response. Deflazacort 6mg Tablets for Duchenne Muscular Dystrophy Deflazacort 6mg Tablets […]
Paracetamol 450mg and Orphenadrine Citrate 35mg Tablets Manufacturer in India India has become a leading hub for pharmaceutical manufacturing, offering world-class formulations, certified production facilities, and competitive pricing for domestic and international markets. We are proud to be recognized as a trusted Paracetamol 450mg and Orphenadrine Citrate 35mg Tablets Manufacturer in India, delivering superior quality products for hospitals, distributors, pharmacies, government tenders, and private healthcare institutions. Our advanced manufacturing systems, strict quality assurance protocols, and international export capabilities allow us to serve customers across Africa, the Middle East, LATAM, Asia, and global regulated markets. We focus on innovation, consistency, and timely delivery while maintaining international pharmaceutical standards. Paracetamol 450mg and Orphenadrine Citrate 35mg Tablets – Product Overview Paracetamol 450mg and Orphenadrine Citrate 35mg Tablets Paracetamol 450mg and Orphenadrine Citrate 35mg Tablets are widely prescribed for the management of acute painful musculoskeletal conditions, stiffness, and muscle spasms. This combination is highly effective where pain relief and muscle relaxation are required together. Composition Paracetamol 450mg Orphenadrine Citrate 35mg Dosage Form Oral Tablets Blister Pack / Alu-Alu Pack / Strip Pack Bulk Packaging Available for Export Brand Name ORPETAJ This formulation is manufactured under stringent GMP norms to ensure purity, safety, stability, and […]
Ribavirin Capsules 200mg Manufacturer in India Ribavirin Capsules 200mg Manufacturer in India We are recognized as a reliable Ribavirin Capsules 200mg manufacturer in India, offering premium-quality antiviral formulations manufactured under strict pharmaceutical standards. Our Ribavirin Capsules are produced in WHO-GMP compliant facilities using advanced technology, ensuring superior purity, consistent potency, and excellent stability. We serve domestic and international markets with dependable manufacturing, bulk supply, third-party manufacturing, and export services. Ribavirin Capsules 200mg are widely used in combination therapies for the treatment of chronic Hepatitis C Virus (HCV) infection and selected viral conditions under medical supervision. We focus on precision manufacturing, quality assurance, and timely delivery, making us a preferred pharmaceutical partner across India, Africa, the Middle East, and Latin America. What is Ribavirin Capsules 200mg? Ribavirin Capsules Ribavirin Capsules 200mg contain Ribavirin, a broad-spectrum antiviral medicine used primarily in combination with other medications for chronic hepatitis C treatment. It works by inhibiting viral replication, helping reduce viral load and supporting successful treatment outcomes. The medicine is generally prescribed as part of a combination regimen and should be taken only under qualified medical guidance. Our manufacturing process ensures that every capsule meets pharmacopeial quality standards and global compliance requirements. Ribavirin Capsules […]
Potassium Iodate Tablets 85mg Manufacturer in India India has emerged as a global pharmaceutical hub, offering reliable manufacturing solutions for essential medicines and specialty formulations. Among the leading names in this segment, Taj Pharma is recognized as a trusted Potassium Iodate Tablets 85mg manufacturer in India, delivering high-quality formulations for domestic and international markets. With advanced production facilities, strict quality systems, and worldwide export capabilities, we provide dependable Potassium Iodate Tablets 85mg to healthcare institutions, government agencies, distributors, and pharmaceutical buyers. Leading Potassium Iodate Tablets 85mg Manufacturer in India Potassium Iodate Tablets 85mg We specialize in manufacturing Potassium Iodate Tablets 85mg under stringent pharmaceutical standards to ensure purity, stability, and efficacy. Our manufacturing units follow GMP-compliant processes and are equipped with modern machinery for precision tablet compression, coating, packaging, and quality inspection. Potassium Iodate Tablets 85mg are widely used in public health initiatives, emergency preparedness programs, iodine supplementation strategies, and industrial applications where pharmaceutical-grade iodine formulations are required. As a reputed Potassium Iodate Tablets 85mg manufacturer supplier in India, we focus on: Accurate dosage formulation Pharmaceutical-grade raw materials Batch consistency Long shelf life Moisture-protected packaging Export-standard labeling Potassium Iodate Tablets 85mg Exporter from India We serve clients across Africa, the […]
Dexamethasone Tablets 0.5mg Manufacturer in India Introduction to Dexamethasone Tablets 0.5mg We are a leading Dexamethasone Tablets 0.5mg manufacturer in India, delivering high-quality pharmaceutical formulations under the trusted brand name DEXOTAJ. Our formulation is widely recognized for its effectiveness in managing a wide range of inflammatory and autoimmune conditions. Dexamethasone is a potent corticosteroid that helps control inflammation, allergic reactions, and immune system overactivity. Manufactured in WHO-GMP certified facilities, our tablets are designed to meet stringent international quality standards, ensuring safety, efficacy, and purity for global healthcare needs. Trusted Manufacturer, Exporter & Supplier of Dexamethasone Tablets 0.5mg in India Dexamethasone Tablets 0.5mg We are a reputed pharmaceutical company based in Vapi, Gujarat, India, specializing in the manufacturing, export, and supply of Dexamethasone Tablets 0.5mg. Our strong distribution network enables us to serve clients across India and international markets including: Africa Middle East Latin America (LATAM) Southeast Asia CIS countries Our commitment to quality and timely delivery has made us a preferred partner for healthcare providers, distributors, and PCD pharma franchise businesses worldwide. Therapeutic Uses of Dexamethasone Tablets 0.5mg Dexamethasone Tablets 0.5mg are widely prescribed for their strong anti-inflammatory and immunosuppressant properties. The medicine is effective in managing several medical conditions, […]
Paroxetine Tablets Manufacturer in India Paroxetine 12.5mg Tablets Manufacturer in India We are recognized as a reliable Paroxetine 12.5mg Tablets manufacturer in India, delivering high-quality pharmaceutical formulations for domestic and international markets. Our manufacturing operations are designed to meet stringent quality standards, ensuring every batch of Paroxetine Extended-release Tablets offers consistent composition, purity, and performance. With advanced production facilities in Vapi, Gujarat, we supply Paroxetine 12.5mg Tablets across PAN India and export to Africa, the Middle East, LATAM, Asia, and regulated markets. Our focus remains on quality manufacturing, timely delivery, competitive pricing, and long-term business partnerships. What Are Paroxetine 12.5mg Tablets? Paroxetine Tablets 12.5mg Paroxetine 12.5mg Tablets are extended-release antidepressant tablets widely prescribed for managing mental health conditions. These tablets belong to the SSRI (Selective Serotonin Reuptake Inhibitor) category and are commonly used to help improve serotonin levels in the brain. Paroxetine Extended-release Tablets are generally prescribed for: Major depressive disorder Panic disorder Social anxiety disorder Generalized anxiety disorder Obsessive-compulsive disorder Premenstrual dysphoric disorder The controlled-release formulation allows gradual release of the active ingredient, helping maintain therapeutic levels over time. Paroxetine 12.5mg Tablets Manufacturer Supplier and Exporter As an established Paroxetine 12.5mg Tablets manufacturer supplier and exporter, we support wholesalers, […]
Paroxetine 20mg Tablets Manufacturer in India Paroxetine 20mg Tablets by Taj Pharma – Reliable Manufacturing Excellence from India We are a trusted Paroxetine 20mg Tablets manufacturer in India, delivering premium pharmaceutical products that meet stringent quality standards for domestic and international markets. Our advanced production facilities, experienced formulation teams, and commitment to regulatory compliance make us a preferred partner for buyers seeking dependable sourcing of Paroxetine Tablets 20mg. Paroxetine is widely prescribed for the treatment of depression, panic disorder, anxiety disorder, obsessive-compulsive disorder (OCD), social phobia, post-traumatic stress disorder (PTSD), and related psychiatric conditions. As a leading manufacturer, we ensure every batch is produced with precision, consistency, and high-grade active ingredients. What is Paroxetine 20mg Tablet? Paroxetine 20mg Tablets (btn) Paroxetine belongs to the class of medicines known as Selective Serotonin Reuptake Inhibitors (SSRIs). It works by increasing serotonin levels in the brain, helping improve mood, emotional stability, sleep quality, and mental well-being. Paroxetine 20mg Tablets are commonly recommended by healthcare professionals for: Major depressive disorder Generalized anxiety disorder Panic disorder Obsessive-compulsive disorder Social anxiety disorder PTSD Premenstrual dysphoric disorder We manufacture Paroxetine Tablets in compliance with pharmacopoeial standards, ensuring therapeutic effectiveness and patient safety. Why Choose Us as Paroxetine […]
Paroxetine Tablets Manufacturer in India Paroxetine 12.5mg Tablets Manufacturer in India We are recognized among the leading Paroxetine 12.5mg Tablets manufacturers in India, delivering premium-quality pharmaceutical products that meet domestic and international healthcare standards. Our manufacturing facilities are equipped with advanced machinery, modern quality systems, and strict compliance processes to ensure every tablet maintains consistent potency, safety, and effectiveness. Paroxetine 12.5mg Tablets are widely prescribed for the treatment of depression, panic disorder, obsessive-compulsive disorder, social anxiety disorder, generalized anxiety disorder, and other mood-related conditions. As a trusted manufacturer and exporter, we supply high-quality formulations designed to support patient well-being while maintaining stringent pharmaceutical standards. Paroxetine 12.5mg Tablets Supplier in India Paroxetine 12.5mg Tablets We supply Paroxetine 12.5mg Tablets across PAN India with reliable logistics, secure packaging, and timely dispatch services. Hospitals, wholesalers, pharmacies, healthcare distributors, and institutional buyers choose us for our commitment to quality and uninterrupted product availability. Our supply network covers: Mumbai Maharashtra Gujarat Delhi Karnataka Tamil Nadu Telangana Andhra Pradesh Uttar Pradesh Rajasthan West Bengal Punjab We maintain stock readiness and streamlined order management systems for fast fulfillment. Trusted Exporter of Paroxetine 12.5mg Tablets to Global Markets We are an experienced Paroxetine 12.5mg Tablets exporter from India, […]
Clozapine 25mg Tablets Manufacturer Supplier in India Clozapine 25mg Tablets Manufacturer in India We are recognized among the trusted Clozapine 25mg Tablets manufacturers in India, delivering high-quality pharmaceutical formulations that meet domestic and international standards. Our advanced manufacturing facilities, strict quality systems, and commitment to regulatory compliance make us a preferred partner for hospitals, distributors, wholesalers, and healthcare institutions worldwide. Clozapine 25mg Tablets are widely prescribed for the management of treatment-resistant schizophrenia and related psychiatric conditions. As a responsible pharmaceutical manufacturer, we ensure every batch is produced with precision, purity, and consistency. Our focus remains on delivering reliable formulations that healthcare professionals can trust. What Are Clozapine 25mg Tablets? Clozapine 25mg Tablets (Baw) Clozapine belongs to the class of atypical antipsychotic medicines. It is used primarily when other antipsychotic medications have not shown sufficient clinical response. Clozapine 25mg Tablets help in reducing symptoms such as hallucinations, severe mood disturbances, disorganized thinking, agitation, and social withdrawal. This medicine works by balancing neurotransmitters in the brain, especially dopamine and serotonin pathways. With regular medical supervision, Clozapine can significantly improve mental stability and quality of life. Top Clozapine 25mg Tablets Manufacturer from Gujarat India We manufacture Clozapine 25mg Tablets in Gujarat, India, using […]
Glimepiride 1mg, Metformin 500mg and Voglibose 0.2mg Tablet Manufacturer Supplier in India Glimepiride, Metformin and Voglibose Tablet Manufacturer in India We are a reputed manufacturer, exporter, and supplier of Glimepiride 1mg, Metformin 500mg and Voglibose 0.2mg Tablet in India, delivering reliable pharmaceutical formulations for domestic and international markets. This triple-combination antidiabetic tablet is widely prescribed for the management of Type 2 Diabetes Mellitus in patients who require multi-target glycemic control. Manufactured in advanced WHO-GMP compliant facilities in Gujarat, India, our tablets are developed under stringent quality systems to ensure safety, efficacy, stability, and consistent therapeutic performance. We supply bulk quantities, private label orders, contract manufacturing solutions, and regulated export consignments for buyers worldwide. Composition of Glimepiride 1mg, Metformin 500mg and Voglibose 0.2mg Tablet Glimepiride 1mg, Metformin 500mg and Voglibose 0.2mg Tablet Each tablet contains: Glimepiride 1mg Metformin Hydrochloride 500mg Voglibose 0.2mg This balanced formulation supports comprehensive blood sugar control by addressing multiple metabolic pathways involved in diabetes. How This Triple Combination Works Glimepiride 1mg Glimepiride belongs to the sulfonylurea class and stimulates insulin release from pancreatic beta cells. It helps reduce fasting and post-meal blood glucose levels. Metformin 500mg Metformin decreases hepatic glucose production, improves insulin sensitivity, and enhances peripheral […]
Escitalopram Tablets Manufacturer in India Escitalopram 5mg Tablets Manufacturer in India We are a leading Escitalopram 5mg Tablets manufacturer in India, delivering premium-quality psychiatric and neurological medicines for domestic and international markets. Taj Pharma is recognized for manufacturing high-purity pharmaceutical formulations under strict quality standards, ensuring effective treatment solutions for healthcare providers, hospitals, pharmacies, distributors, and importers worldwide. Escitalopram 5mg Tablets are widely prescribed for the treatment of major depressive disorder, generalized anxiety disorder, panic disorder, obsessive-compulsive disorder, social anxiety disorder, and stress-related mental health conditions. We manufacture these tablets using advanced technology and pharmaceutical-grade raw materials to maintain stability, safety, and efficacy. Our manufacturing operations are backed by modern facilities, experienced formulation scientists, robust quality assurance systems, and efficient logistics support, making us a preferred global source for Escitalopram products. What is Escitalopram 5mg Tablets? Escitalopram 5mg Tablets (Escitaj) Escitalopram 5mg Tablets belong to the class of medicines known as Selective Serotonin Reuptake Inhibitors (SSRIs). This medicine works by increasing serotonin activity in the brain, helping improve mood balance, emotional stability, and anxiety control. Escitalopram 5mg is commonly prescribed as an initial or maintenance dosage depending on patient requirements. It is often recommended for: Depression Anxiety disorders Panic attacks […]
Sodium Valproate and Valproic Acid Manufacturer Supplier in India Sodium Valproate 200mg and Valproic Acid 87mg Manufacturer in India We are recognized among the leading manufacturers and exporters of Sodium Valproate 200mg and Valproic Acid 87mg tablets in India, delivering pharmaceutical excellence through advanced manufacturing systems, strict quality assurance, and global supply capability. Our facilities in India operate under international standards to provide safe, effective, and high-purity formulations for domestic and overseas healthcare markets. Sodium Valproate and Valproic Acid combination tablets are widely prescribed for the management of epilepsy, seizure disorders, and bipolar disorder. This formulation supports long-term neurological care by helping stabilize electrical activity in the brain and reducing recurrent seizures. Our commitment to quality, timely delivery, and affordable pricing has made us a preferred Sodium Valproate manufacturer in India, supplying regulated and semi-regulated markets worldwide. What is Sodium Valproate 200mg and Valproic Acid 87mg? Sodium Valproate 200mg and Valproic Acid 87mg Sodium Valproate and Valproic Acid is a clinically established combination medicine used for: Epilepsy and seizure control Generalized tonic-clonic seizures Partial seizures Bipolar affective disorder Prevention of recurrent neurological episodes Long-term maintenance therapy under physician supervision This medicine works by increasing the level of calming neurotransmitters in […]
Escitalopram 10mg Tablets Manufacturer Supplier in India Escitalopram 10mg Tablets Manufacturer in India We are recognized as a trusted Escitalopram 10mg Tablets manufacturer in India, delivering premium-quality pharmaceutical formulations for domestic and international markets. With advanced manufacturing facilities, strict quality assurance systems, and a commitment to global healthcare standards, we supply reliable Escitalopram Tablets to hospitals, distributors, pharmacies, government tenders, and healthcare organizations worldwide. Escitalopram 10mg Tablets are widely prescribed for the treatment of depression, anxiety disorders, panic disorder, obsessive-compulsive disorder, and generalized anxiety conditions. As a reputed manufacturer and exporter, we ensure every batch is produced with precision, purity, and consistency. What is Escitalopram 10mg Tablets? Escitalopram 10mg Tablets (Escitaj) Escitalopram belongs to the selective serotonin reuptake inhibitor (SSRI) class of medicines. It works by increasing serotonin levels in the brain, helping stabilize mood, reduce nervousness, improve sleep, and restore emotional balance. Doctors commonly prescribe Escitalopram 10mg Tablets for: Major depressive disorder Generalized anxiety disorder Panic disorder Social anxiety disorder Obsessive-compulsive disorder Stress-related emotional imbalance This medicine is considered one of the preferred antidepressants due to its effectiveness and favorable tolerability profile. Why We Are a Preferred Escitalopram Tablets Manufacturer We maintain world-class pharmaceutical production systems that make us […]
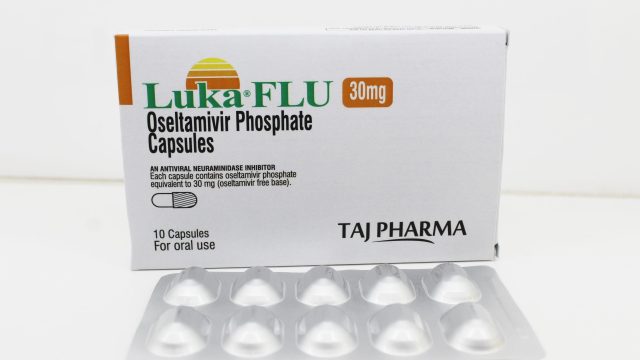
Oseltamivir Phosphate Capsules Manufacturer in India Oseltamivir Phosphate Capsules 30mg We are a leading manufacturer and exporter of Oseltamivir Phosphate Capsules 30mg, delivering high-quality antiviral formulations designed for the treatment and prevention of influenza infections. Our commitment to pharmaceutical excellence ensures that every capsule meets stringent international quality standards, making us a preferred partner for global healthcare providers. Oseltamivir is a potent antiviral agent widely prescribed for managing influenza A and B viruses. It works by inhibiting the neuraminidase enzyme, which plays a crucial role in viral replication and spread within the human body. By blocking this enzyme, the medicine effectively limits the progression of infection and reduces symptom severity. Mechanism of Action and Therapeutic Benefits Oseltamivir Capsules 30mg (LukaFLU) Oseltamivir Phosphate Capsules 30mg function as a neuraminidase inhibitor. This mechanism prevents newly formed viruses from spreading to healthy cells, thereby controlling infection at an early stage. Key Benefits: Reduces the duration of flu symptoms Minimizes severity of infection Helps prevent complications such as bronchitis and pneumonia Effective in both treatment and prophylaxis Suitable for adults and pediatric patients with adjusted dosing Early administration, ideally within 48 hours of symptom onset, significantly enhances the effectiveness of the medication. Indications and […]
Oseltamivir Phosphate Capsules 75mg Manufacturer in India Oseltamivir Phosphate Capsules 75mg Manufacturer in India We are recognized as a trusted and established manufacturer of Oseltamivir Phosphate Capsules 75mg in India, delivering consistent quality, efficacy, and global compliance. Our advanced pharmaceutical manufacturing infrastructure and strict quality control systems enable us to supply premium antiviral formulations across domestic and international markets. Our product, widely known under the brand name LukaFLU, is manufactured using high-grade active pharmaceutical ingredients (APIs) and follows WHO-GMP standards. We ensure that every batch meets stringent regulatory requirements, making us a reliable partner for distributors, hospitals, and government institutions worldwide. What is Oseltamivir Phosphate 75mg and How It Works Oseltamivir Phosphate Capsules 75mg Oseltamivir Phosphate is a potent antiviral medication used for the treatment and prevention of influenza (flu), including both influenza A and influenza B viruses. It belongs to a class of drugs known as neuraminidase inhibitors. We formulate Oseltamivir 75mg capsules to block the action of the neuraminidase enzyme, which is essential for viral replication. By inhibiting this enzyme, the medicine prevents the virus from spreading to healthy cells, thereby reducing the severity and duration of flu symptoms. Therapeutic Uses of Oseltamivir Capsules 75mg We supply Oseltamivir […]
Ivermectin 2mg and Praziquantel 50mg Tablets Manufacturer in India Introduction to Ivermectin and Praziquantel Combination Tablets We are a leading manufacturer, exporter, and supplier of Ivermectin 2mg and Praziquantel 50mg Tablets (Iveropraz) in India, offering world-class veterinary pharmaceutical solutions designed to ensure effective protection against endoparasitic infections in companion animals. Our formulation is specifically developed for dogs and cats suffering from mixed worm infestations, delivering broad-spectrum deworming efficacy in a single, reliable dosage form. This combination therapy plays a vital role in modern veterinary medicine by targeting both nematodes and cestodes, ensuring complete parasite elimination and improved animal health outcomes. With strict adherence to international manufacturing standards, we ensure consistent quality, safety, and therapeutic effectiveness in every batch. High-Quality Manufacturing Standards in India Ivermectin 2mg and Praziquantel 50mg Tablets We operate as a GMP-WHO certified pharmaceutical manufacturer based in India, ensuring that every stage of production meets stringent global regulatory requirements. Our Ivermectin and Praziquantel Tablets are produced under controlled environments using advanced technology, validated processes, and high-purity raw materials sourced from trusted global suppliers. Our manufacturing facility follows: WHO-GMP certified production protocols ISO-compliant quality assurance systems Advanced formulation and blending technology Strict microbiological and chemical testing Real-time stability and […]
Orlistat Capsules 120mg Manufacturer in India Orlistat Capsules 120mg Manufacturer in India We at Taj Pharma India are a globally recognized manufacturer, exporter, and supplier of high-quality pharmaceutical formulations, including Orlistat Capsules 120mg. With advanced manufacturing infrastructure and strict adherence to international quality standards, we deliver consistent, safe, and effective weight management solutions to healthcare markets across the world. Our strong presence in regulated and semi-regulated markets has positioned us as a reliable partner for Orlistat Capsules 120mg manufacturing in India, serving regions such as Africa, the Middle East, and Latin America with premium pharmaceutical products. About Orlistat Capsules 120mg (Anti-Obesity Medicine) Orlistat Capsules 120mg (Fetrasil) Orlistat Capsules 120mg are widely prescribed anti-obesity medications used to support weight reduction in overweight and obese patients. This medication works by reducing the absorption of dietary fats in the body, thereby lowering overall calorie intake. We manufacture Orlistat Capsules under strict quality control to ensure optimal therapeutic performance. When used along with a balanced diet and lifestyle modification, it helps patients achieve sustainable weight loss outcomes. Orlistat is typically administered orally during or after meals containing fat, ensuring effective action within the gastrointestinal tract. Mechanism of Action of Orlistat Capsules 120mg We ensure […]
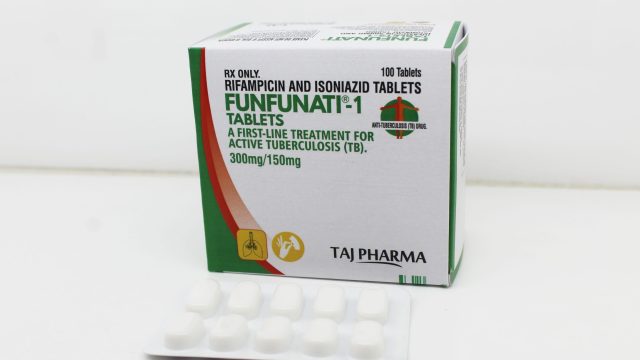
Rifampicin 300mg and Isoniazide 150mg Tablets Manufacturer in India Leading Manufacturer of Rifampicin 300mg and Isoniazide 150mg Tablets (FUNFUNATI-1) We are a globally recognized pharmaceutical company specializing in the manufacturing, export, and supply of Rifampicin 300mg and Isoniazide 150mg Tablets (FUNFUNATI-1). With advanced production facilities in Vapi, Gujarat, we ensure the highest standards of quality, safety, and efficacy in every batch we deliver. Our commitment to excellence has positioned us among the most reliable suppliers across India, Africa, the Middle East, and Latin America. Our fixed-dose combination tablets are developed in compliance with WHO-GMP and international regulatory standards, ensuring consistent therapeutic outcomes for patients suffering from tuberculosis. Comprehensive Overview of Rifampicin and Isoniazide Tablets Rifampicin 300mg and Isoniazide 150mg Tablets (FUNFUNATI) Rifampicin 300mg and Isoniazide 150mg Tablets represent a highly effective combination therapy designed for the treatment and prevention of tuberculosis (TB). This formulation integrates two potent first-line anti-tubercular agents that work synergistically to eliminate Mycobacterium tuberculosis and prevent the emergence of drug resistance. Rifampicin acts by inhibiting bacterial RNA synthesis, effectively stopping protein production necessary for bacterial survival. Isoniazide disrupts the formation of the bacterial cell wall, weakening and ultimately destroying the pathogen. Together, these mechanisms ensure rapid bacterial […]
Lopinavir 200mg and Ritonavir 50mg Tablets Manufacturer in Mumbai, India Leading Manufacturer of Lopinavir 200mg and Ritonavir 50mg Tablets in India We are a trusted and established manufacturer, exporter, and supplier of Lopinavir 200mg and Ritonavir 50mg Tablets, delivering globally approved antiviral formulations that meet stringent quality and safety standards. Our manufacturing excellence is centered in India, with strong operational presence in major pharmaceutical hubs including Mumbai and Vapi. We specialize in producing high-quality antiretroviral medicines used in the treatment of HIV-1 infection. Our formulation of Lopinavir and Ritonavir is designed to ensure maximum therapeutic efficiency, stability, and patient compliance. About Lopinavir 200mg and Ritonavir 50mg Tablets Lopinavir 200mg and Ritonavir 50mg Tablets (Kyazilitaj) Lopinavir 200mg and Ritonavir 50mg Tablets are a fixed-dose combination antiretroviral medication widely used in the management of HIV infection. Lopinavir acts as a protease inhibitor, while Ritonavir enhances its effectiveness by boosting plasma concentration. This combination works by inhibiting the protease enzyme required for viral replication, thereby reducing the viral load in the body and slowing the progression of HIV-1 infection. Our manufacturing process ensures precise dosing, high bioavailability, and consistent therapeutic performance. Trusted Pharmaceutical Manufacturer We operate under a globally recognized pharmaceutical manufacturing infrastructure […]
Abacavir 300mg (Triuvato) Manufacturer in India Premium Quality Abacavir 300mg Tablets from India We are recognized as a trusted manufacturer and global exporter of Abacavir 300mg (Triuvato), delivering consistent pharmaceutical excellence across regulated and semi-regulated markets. Our manufacturing facilities are equipped with advanced technology and adhere strictly to international quality standards, ensuring high purity, safety, and efficacy in every tablet. Abacavir 300mg is a widely prescribed antiretroviral medication used for the treatment of Human Immunodeficiency Virus (HIV-1) infection. As a reliable supplier, we ensure uninterrupted availability of this essential medication across Africa, the Middle East, and Latin America (LATAM), supporting global healthcare systems with dependable pharmaceutical solutions. What is Abacavir 300mg and Its Medical Use Abacavir Tablets 300mg Abacavir belongs to the class of nucleoside reverse transcriptase inhibitors (NRTIs). It plays a critical role in antiretroviral therapy (ART) by inhibiting the replication of the HIV virus in human cells. This prevents the virus from multiplying and reduces viral load, improving immune function and overall patient outcomes. In addition to HIV-1 treatment, Abacavir is sometimes used in combination therapies under strict medical supervision. It is not a cure but significantly enhances quality of life when used as part of a comprehensive […]
Rifampin Injection 600mg (RIFLITAJ) Manufacturer, Supplier & Exporter in India Leading Rifampin Injection 600mg Manufacturer in India We are recognized as a trusted and established manufacturer, supplier, and exporter of Rifampin Injection 600mg (RIFLITAJ) in India. With advanced manufacturing facilities and strict quality control protocols, we ensure that every batch meets international pharmaceutical standards. Our production unit in Vapi, Gujarat is equipped with state-of-the-art technology, enabling us to deliver consistent quality formulations for global markets. Our expertise in manufacturing Rifampin Injection 600mg allows us to serve clients across India as well as export markets including Africa, the Middle East, and Latin America. We maintain a strong commitment to quality, compliance, and customer satisfaction. What is Rifampin Injection 600mg (RIFLITAJ)? Rifampin 600mg (RIFLITAJ) Rifampin Injection 600mg is a potent antibiotic widely used in the treatment of serious bacterial infections, especially tuberculosis (TB). It belongs to the rifamycin class of antibiotics and works by inhibiting bacterial RNA synthesis, effectively stopping the growth and multiplication of bacteria. This injectable formulation is particularly useful in hospital settings where oral administration may not be feasible or when rapid therapeutic action is required. It is often included as part of combination therapy for tuberculosis and other […]
Primaquine Tablets 7.5mg Manufacturer in India Leading Primaquine Tablets 7.5mg Manufacturer PAN India We are a globally recognized manufacturer, supplier, and exporter of Primaquine Tablets 7.5mg in India, delivering superior pharmaceutical formulations with guaranteed quality, purity, and consistency. As a leading name in the industry, we specialize in providing high-demand antimalarial medications across PAN India and international markets including Africa, the Middle East, and Latin America. Our commitment to excellence has positioned us as a top Primaquine 7.5mg manufacturer from Mumbai and Vapi, Gujarat, offering reliable supply chains, regulatory compliance, and competitive pricing for global buyers. Premium Quality Primaquine Tablets 7.5mg – Assured Purity and Effectiveness Primaquine Tablets 7.5mg We manufacture Primaquine Tablets 7.5mg using advanced pharmaceutical technology and strict quality control systems. Each tablet is formulated to ensure optimal therapeutic efficacy, making it highly effective in malaria treatment protocols. Key Product Highlights: High-quality API sourcing for maximum purity Accurate dosage formulation (7.5mg strength) WHO-GMP certified manufacturing process Stable shelf life with protective packaging Batch-to-batch consistency Our products are trusted by healthcare providers for their reliable performance and safety standards. Mechanism of Action and Therapeutic Benefits Primaquine Tablets 7.5mg are widely prescribed for the treatment and prevention of malaria. The […]
Dolutegravir Tablets 10mg Manufacturer & Supplier in India Introduction to Dolutegravir Tablets 10mg We are a leading manufacturer, exporter, and supplier of Dolutegravir Tablets 10mg in India, delivering high-quality pharmaceutical formulations that meet global healthcare standards. Dolutegravir is a widely prescribed antiretroviral medication used in the effective management of HIV-1 infection. It belongs to the integrase inhibitor class, which works by preventing the virus from multiplying within human cells, thereby reducing viral load and improving immune function. Our commitment to quality, safety, and innovation ensures that our Dolutegravir formulations meet stringent regulatory requirements for international markets including Africa, the Middle East, and Latin America. What Are Dolutegravir Tablets 10mg Used For? Dolutegravir Tablets 10mg are primarily used in combination with other antiretroviral agents for the treatment of HIV infection. These tablets are especially beneficial for: Pediatric patients aged 4 weeks and above Patients weighing at least 3 kg Individuals requiring precise dosing based on body weight The dispersible formulation, often strawberry-flavored, allows for easy oral suspension, making it ideal for children and patients with swallowing difficulties. Mechanism of Action of Dolutegravir Dolutegravir Tablets 10mg Dolutegravir works by inhibiting the integrase enzyme, which is essential for the replication of HIV. By […]
Paroxetine Extended-Release Tablets 20mg Manufacturer Supplier in India Leading Manufacturer of Paroxetine Extended-Release Tablets 20mg in India We are recognized as a reliable and quality-driven manufacturer, supplier, and exporter of Paroxetine Extended-Release Tablets 20mg in India. With a strong manufacturing base in Vapi, Gujarat, we ensure consistent production of high-quality pharmaceutical formulations that meet stringent global standards. Our commitment to excellence, innovation, and compliance has enabled us to serve a wide network of clients across India and international markets including Africa, the Middle East, and Latin America (LATAM). Paroxetine Extended-Release Tablets 20mg are formulated using advanced pharmaceutical technologies to ensure controlled release, optimal efficacy, and improved patient compliance. We strictly adhere to WHO-GMP guidelines and international regulatory requirements, ensuring that every batch meets global quality benchmarks. What is Paroxetine Extended-Release Tablets 20mg? Paroxetine Extended-release Tablets 20mg Paroxetine Extended-Release Tablets 20mg belong to the class of antidepressants known as Selective Serotonin Reuptake Inhibitors (SSRIs). These tablets are specifically designed to release the active ingredient gradually, providing sustained therapeutic effects over time. Paroxetine works by increasing serotonin levels in the brain, a neurotransmitter responsible for regulating mood, emotions, and mental stability. This mechanism helps in improving mood and reducing symptoms associated with […]
In today’s evolving healthcare landscape, skin and intimate health conditions are among the most frequently reported concerns across clinics in India. From fungal and vaginal infections to acne, aging skin, scalp disorders, and inflammatory conditions, patients are seeking safe, effective, and clinically validated solutions. At the forefront of this transformation is Taj Pharma India Ltd.—delivering a comprehensive derma and gynaec care portfolio built on scientific research, regulatory compliance, and patient-centric innovation. 🔬 A Comprehensive, Clinically Aligned Product Portfolio Taj Pharma offers an integrated range of products designed to support dermatologists, gynaecologists, hospitals, and skin clinics in addressing diverse patient needs: Anti-fungal creams for vaginal and skin infections Gynaecological care formulations for intimate health management Acne treatment creams & gels targeting mild to severe conditions Medicated anti-lice shampoos for scalp hygiene and infestation control Anti-aging creams promoting skin rejuvenation and elasticity Pain relief gels for musculoskeletal and inflammatory conditions Hydrocortisone creams & dermatological ointments for inflammation and allergies Hand sanitizers & hygiene products supporting infection control Each formulation is developed with a focus on efficacy, safety, and patient compliance, ensuring better clinical outcomes. 👩⚕️ Patient-Centric Care Meets Clinical Excellence Modern patients demand more than just treatment—they expect visible results, minimal side […]
What is Potassium Iodide and Its Role in Radiation Protection Potassium Iodide Tablets USP are globally recognized as a critical pharmaceutical solution for thyroid protection during radiation exposure. In nuclear emergencies, radioactive iodine—especially iodine-131—poses a significant health risk when inhaled or ingested. The human thyroid gland rapidly absorbs iodine, making it particularly vulnerable. Potassium iodide (KI) works by saturating the thyroid gland with stable iodine, thereby preventing the uptake of radioactive iodine. This mechanism significantly reduces the risk of thyroid cancer, thyroid dysfunction, and long-term radiation-induced complications. The effectiveness of KI tablets for radiation protection depends on timely administration, ideally before or immediately after exposure. When used correctly, KI offers up to 24 hours of protection, making it an essential component of nuclear emergency preparedness programs worldwide. Potassium Iodide Tablets USP by Taj Pharma Taj Pharma India is a leading WHO-GMP certified potassium iodide tablets manufacturer and exporter, delivering high-quality, USP-compliant formulations for global markets. Our expertise in pharmaceutical manufacturing ensures that every batch meets stringent international standards for safety, efficacy, and stability. We offer: Potassium Iodide Tablets USP 65 mg Potassium Iodide Tablets USP 130 mg These strengths are aligned with international dosing guidelines, making them suitable for adults, […]
Reliable Supply, Affordable Pricing & Quality Assurance from Taj Pharma India’s healthcare system relies heavily on private doctors, clinics, and nursing homes that provide essential medical services to millions of patients every day. However, many healthcare practitioners face serious challenges in medicine procurement, including supply shortages, fluctuating prices, inconsistent quality, and delayed deliveries from distributors. To address these challenges, Taj Pharma India is inviting doctors, private practitioners, clinics, and nursing home owners across PAN India to procure medicines directly from the manufacturer, ensuring cost efficiency, reliable supply, and consistent quality. Why Direct Procurement from the Manufacturer Matters Most doctors and clinics purchase medicines through multiple distributor layers, which often leads to: Increased procurement costs Unpredictable stock availability Delayed deliveries Quality concerns from unknown sources Inventory management problems By purchasing directly from Taj Pharma India Ltd., healthcare providers can eliminate unnecessary intermediaries, ensuring better pricing, dependable supply, and improved inventory control. Taj Pharma – Trusted Pharmaceutical Manufacturer With over 30 years of experience in pharmaceutical manufacturing, Taj Pharma has built a strong reputation in domestic and international markets for producing high-quality, GMP-compliant medicines. The company operates modern manufacturing facilities producing a wide range of pharmaceutical formulations suitable for hospital, clinic, and […]
A Public Health Preparedness Perspective for Ministries of Health In times of geopolitical uncertainty and rising regional tensions, public health preparedness becomes a critical responsibility of governments. Among the emergency countermeasures recommended globally for radiological incidents is the strategic stockpiling and distribution of Potassium Iodide tablets, which are widely recognized for protecting the thyroid gland from radioactive iodine exposure. This measure has been adopted in many developed nations as part of nuclear emergency planning to protect civilians, children, and frontline responders. For the Middle East and North Africa (MENA) region, where populations are dense and critical infrastructure is concentrated, early planning and preparedness can save millions of lives. Why Potassium Iodide Is Important During a nuclear or radiological incident, radioactive iodine (I-131) may be released into the environment. When inhaled or ingested, it accumulates in the thyroid gland and may significantly increase the risk of thyroid cancer. Potassium iodide tablets work by saturating the thyroid with stable iodine, preventing the absorption of radioactive iodine. Key benefits include: • Reduces thyroid cancer risk• Protects children and pregnant women• Low cost and easy mass distribution• Long shelf life for national emergency stockpiles• Effective if taken before or shortly after exposure International agencies […]
The Middle East and North Africa (MENA), Iran, and Gulf nations represent one of the most dynamic yet complex healthcare regions in the world. Countries such as Saudi Arabia, United Arab Emirates, Qatar, Kuwait, Bahrain, Oman, Iran, Iraq, Jordan, Lebanon, Syria, Yemen, Egypt, Morocco, Algeria, Tunisia, Libya, Sudan, and others face diverse healthcare challenges driven by population growth, climate change, regional instability, and the increasing burden of chronic diseases. In such a rapidly evolving environment, reliable access to quality medicines, emergency preparedness drugs, and specialty therapeutics has become essential for healthcare systems, governments, humanitarian organizations, and medical distributors across the region. Healthcare Challenges Across the MENA and Gulf Regions 1. Rising Chronic Diseases and Lifestyle Disorders Many Gulf countries are witnessing a sharp rise in diabetes, cardiovascular disease, hypertension, and obesity, driven by urban lifestyles and dietary changes. These conditions require long-term treatment, preventive care, and continuous pharmaceutical supply. 2. Climate and Environmental Health Risks Environmental factors increasingly affect public health in the region. Dust storms originating from North Africa and the Middle East impact hundreds of millions of people globally, contributing to respiratory diseases and cardiovascular complications. Extreme heat events, which are intensifying due to climate change, are also […]
Regulatory Process, Documentation, Timelines & Compliance By Taj Pharma India Ltd. Azerbaijan is an important and fast-growing pharmaceutical market in the CIS region. To legally import, distribute, and market external (topical) non-sterile pharmaceutical preparations such as creams, ointments, gels, lotions, and topical solutions, prior product registration and marketing authorization is mandatory. Taj Pharma India Ltd., a WHO-GMP and EU-GMP compliant Indian pharmaceutical manufacturer, provides comprehensive regulatory and documentation support for successful registration of topical formulations in Azerbaijan. Regulatory Authority in Azerbaijan Pharmaceutical product registration in Azerbaijan is governed by the: Ministry of Health of the Republic of Azerbaijanthrough the Analytical Expertise Center (AEC) The AEC is responsible for: Evaluation of quality, safety, and efficacy Registration and re-registration of medicinal products Regulatory review of imported pharmaceuticals Verification of GMP compliance Only products granted Marketing Authorization may be legally marketed in Azerbaijan. Product Scope – External Preparations External preparations are regulated as medicinal products when they carry therapeutic or preventive claims. Covered non-sterile dosage forms include: Creams Ointments Gels Lotions Topical solutions and suspensions Pastes Products with purely cosmetic claims fall under separate cosmetic regulations and require a different approval pathway. Eligibility & Applicant Requirements Foreign manufacturers may register products in Azerbaijan […]
Leading Manufacturer and Exporter of Choline Fenofibrate Delayed Release Tablets 135mg in India Assured Quality and Purity in Choline Fenofibrate Delayed Release Tablets 135mg We stand as a trusted and globally recognized pharmaceutical manufacturer, exporter, and supplier of Choline Fenofibrate Delayed Release Tablets 135mg, delivering products that meet the highest standards of quality, safety, and therapeutic efficacy. Taj Pharma India has established a strong presence as a premium manufacturer in Vapi, Gujarat, serving PAN India markets and international destinations including Africa, the Middle East, and LTAM. Our Choline Fenofibrate Delayed Release Tablets are developed using advanced formulation technologies and manufactured in WHO-GMP compliant facilities, ensuring consistent potency, purity, and stability in every batch. This commitment enables us to be recognized among the leading Choline Fenofibrate Delayed Release Tablets manufacturers and suppliers in India. Choline Fenofibrate Delayed Release Tablets 135mg About Choline Fenofibrate Delayed Release Tablets 135mg Choline Fenofibrate is a lipid-lowering medication widely prescribed for the management of high cholesterol and high triglycerides. It plays a vital role in improving lipid profiles by: Lowering triglyceride levels Reducing LDL (bad cholesterol) Increasing HDL (good cholesterol) Our Delayed Release Tablets 135mg are designed to ensure controlled drug release, enhancing bioavailability while minimizing […]
Leading Paracetamol Tablets 500mg Manufacturer, Supplier & Exporter in India Assurance of Quality, Purity, and Global Pharmaceutical Excellence We stand as a trusted and well-established Paracetamol Tablets 500mg manufacturer in India, delivering uncompromising quality, purity, and consistency to domestic and international markets. As Taj Pharma India, headquartered in Vapi, Gujarat, we have built a strong reputation as a manufacturer, exporter, and supplier of finished Paracetamol Tablets 500mg across PAN India, Africa, the Middle East, and LTAM regions. Our commitment to global standards, regulatory compliance, and patient safety positions us among the leading #1 Paracetamol Tablets manufacturers and suppliers in India. What Makes Paracetamol Tablets 500mg Essential in Modern Healthcare Paracetamol Tablets 500mg Paracetamol (Acetaminophen) is one of the most widely used analgesic (pain reliever) and antipyretic (fever reducer) medications worldwide. It works by blocking the release of certain chemical messengers responsible for pain and fever, offering effective relief without causing gastric irritation when used as directed. Our Paracetamol Tablets 500mg are formulated to meet stringent quality benchmarks and are widely prescribed and trusted for managing: Headaches and migraines Toothaches and sore throats Menstrual (period) pain Arthritis and muscle aches Fever associated with infections Symptoms of the common cold and flu […]
Strengthening Healthcare Through India–Turkmenistan Pharmaceutical Cooperation Turkmenistan stands at an important juncture in strengthening its national healthcare infrastructure, with a clear focus on quality medicines, supply security, and long-term sustainability. In this evolving healthcare landscape, international pharmaceutical partnerships play a vital role in ensuring uninterrupted access to essential, safe, and affordable medicines. Taj Pharma India Ltd., a globally oriented pharmaceutical manufacturer from India, emerges as a natural and strategic partner for Turkmenistan, aligning manufacturing excellence with public health priorities and bilateral trade cooperation. India and Turkmenistan: A Foundation of Trusted Bilateral Relations India and Turkmenistan share long-standing diplomatic and economic relations built on mutual respect, cooperation, and shared development goals. Over the years, both countries have actively promoted collaboration across sectors such as energy, infrastructure, education, healthcare, and pharmaceuticals. Pharmaceutical cooperation holds particular importance due to: India’s globally recognized leadership in generic medicines and healthcare manufacturing Turkmenistan’s commitment to strengthening public healthcare delivery The need for reliable, cost-effective, and quality-assured medicines for government and institutional use Within this framework, Taj Pharma India Ltd. contributes as a direct manufacturer, reinforcing India’s role as a dependable healthcare partner for Turkmenistan. Taj Pharma India Ltd.: Manufacturing Excellence from India Taj Pharma India Ltd. […]
Leading Manufacturer, Exporter & Supplier of Miltefosine 50mg Capsules (Impataj) in India Trusted Name in Miltefosine 50mg Capsules Manufacturing We are Taj Pharma India, a well-established and globally trusted manufacturer, exporter, distributor, and supplier of Miltefosine 50mg Capsules (Impataj), based in Vapi, Gujarat, India. With decades of pharmaceutical expertise, we deliver high-quality, safe, and effective Miltefosine Capsules that meet stringent international quality standards. Our commitment to purity, efficacy, and consistency has positioned us as a leading Miltefosine Capsules manufacturer PAN India and worldwide. Miltefosine is a critical antimicrobial agent widely used in the treatment of kala-azar (visceral leishmaniasis), a life-threatening parasitic disease. As a responsible pharmaceutical manufacturer, we ensure that every capsule is produced using advanced manufacturing processes, WHO-GMP compliant facilities, and rigorous quality control systems. Miltefosine 50mg Capsules About Miltefosine 50mg Capsules (Impataj) Miltefosine 50mg Capsules (Impataj) belong to the class of antimicrobial and antiprotozoal agents. This medicine works by interfering with essential proteins and biochemical pathways required for the survival and growth of parasites, ultimately leading to their death. Due to its proven therapeutic effectiveness, Miltefosine has become a gold-standard oral treatment for kala-azar in many regions. We manufacture finished Miltefosine formulations that are stable, bioavailable, and therapeutically […]
Leading Lamivudine Tablets IP 150mg Manufacturer, Supplier & Exporter in India Trusted Manufacturer of Lamivudine Tablets IP 150mg in India We are Taj Pharma India, a well-established manufacturer, exporter, distributor, and supplier of Lamivudine Tablets IP 150mg from Vapi, Gujarat, India. With years of pharmaceutical manufacturing excellence, we deliver high-quality, high-purity Lamivudine Tablets that comply with Indian Pharmacopoeia (IP) standards and global regulatory requirements. Our Lamivudine Tablets IP 150mg are widely supplied across PAN India, as well as exported to Africa, the Middle East, LTAM, and other international markets. We are recognized as a premium Lamivudine Tablets IP supplier and exporter, committed to quality, consistency, and therapeutic reliability. Lamivudine Tablets IP 150mg About Lamivudine Tablets IP 150mg Lamivudine is a potent antiviral medication used extensively in the treatment of chronic Hepatitis B virus (HBV) infection and, in combination with other antiretroviral drugs, for HIV infection management. It works by inhibiting viral replication, preventing the virus from multiplying in human cells, and helping control viral load effectively. Our Lamivudine Tablets IP 150mg are manufactured under strict GMP-certified facilities, ensuring optimal efficacy, stability, and patient safety. Lamivudine Tablets 150mg Mechanism of Action of Lamivudine Lamivudine acts by blocking reverse transcriptase, an enzyme […]
Fenbendazole Tablets 222mg Manufacturer in India – Trusted Global Supplier & Exporter | Taj Pharma Fenbendazole Tablets 222mg Manufacturer in India Taj Pharma is a trusted Fenbendazole Tablets 222mg manufacturer in India, delivering high-quality veterinary pharmaceutical products to distributors, importers, wholesalers, veterinary institutions, and international buyers. With advanced manufacturing capabilities, stringent quality standards, and an export-focused approach, we supply Fenbendazole Tablets 222mg (Fencure) to customers across Africa, the Middle East, Latin America (LATAM), Asia, and other global markets. Manufactured at our facilities in Vapi, Gujarat, India, our Fenbendazole tablets are produced under strict quality management systems to ensure consistency, purity, and compliance with international pharmaceutical standards. We support private labeling, contract manufacturing, bulk supply, and regulatory documentation for global partners. Fenbendazole Tablets 222mg What is Fenbendazole Tablets 222mg? Fenbendazole is a benzimidazole-class anthelmintic (deworming) medicine widely used in veterinary medicine to help control susceptible gastrointestinal parasites in animals. It works by disrupting essential cellular functions in susceptible parasites, leading to their elimination. Fenbendazole has broad-spectrum activity against many common intestinal parasites when used according to veterinary guidance and approved product labeling. Common Veterinary Uses of Fenbendazole Tablets 222mg Fenbendazole is commonly used in veterinary practice for the treatment and control […]
Leading Manufacturer, Exporter, and Supplier of Sodium Valproate 333mg and Valproic Acid 145mg Tablets in India Trusted Excellence in Sodium Valproate and Valproic Acid Tablet Manufacturing We at Taj Pharma India stand as a well-established, globally trusted Manufacturer, Exporter, and Supplier of Sodium Valproate 333mg and Valproic Acid 145mg Tablets from Vapi, Gujarat, India. With a strong commitment to quality, purity, safety, and regulatory compliance, we deliver pharmaceutical formulations that meet the highest international standards. Our Sodium Valproate and Valproic Acid Tablets are widely recognized across PAN India, as well as in Africa, the Middle East, and LTAM markets, making us a preferred partner for healthcare providers and pharmaceutical distributors worldwide. Assurance of High Quality, Purity, and Compliance Sodium Valproate 333 mg and Valproic Acid 145 mg Tablet Quality is not a claim for us—it is a measurable standard. Our Sodium Valproate and Valproic Acid Tablet manufacturing facilities follow WHO-GMP guidelines, ensuring consistency, safety, and therapeutic efficacy in every batch. Each tablet undergoes rigorous quality control testing, including raw material verification, in-process checks, and finished product analysis. This ensures high purity, accurate dosage strength, and optimal stability, essential for effective epilepsy management. About Sodium Valproate 333mg and Valproic Acid 145mg […]
Leading Ivermectin Tablet USP 12mg Manufacturer in India We stand as a trusted and globally recognized Ivermectin Tablet USP 12mg manufacturer, exporter, and supplier in India, delivering pharmaceutical excellence from Vapi, Gujarat to PAN India and international markets including Africa, the Middle East, and LTAM regions. With a commitment to quality, purity, compliance, and consistency, our finished formulations meet stringent USP standards and international regulatory expectations. Our flagship Ivermectin Tablet USP 12mg is formulated to the highest benchmarks, ensuring dependable therapeutic performance and patient safety. As a premium supplier and exporter, we support wholesalers, distributors, hospitals, institutional buyers, and PCD Pharma Franchise partners with scalable manufacturing capacity and reliable supply chains. About Taj Pharma – Pharmaceutical Manufacturing Excellence Ivermectin Tablets 12mg We are a well-established pharmaceutical manufacturer with decades of experience in solid oral dosage forms, operating advanced facilities in Vapi, Gujarat. Our operations are aligned with GMP-compliant systems, robust quality assurance, and process validation frameworks that ensure batch-to-batch uniformity. Our reputation as a top Ivermectin Tablet USP manufacturer in India is built on: USP-grade raw materials Validated manufacturing processes In-process quality controls Comprehensive stability testing Export-ready documentation We consistently deliver high-quality finished Ivermectin tablets that meet global pharmacopoeial standards. […]
Leading Ivermectin Tablet USP 6mg Manufacturer, Supplier & Exporter in India Trusted Ivermectin Tablet USP 6mg Manufacturer from Vapi, Gujarat, India We are Taj Pharma India, a well-established, globally trusted Manufacturer, Exporter, Distributor, and Supplier of Ivermectin Tablet USP 6mg based in Vapi, Gujarat, India. Our commitment to high-quality manufacturing, international regulatory compliance, and pharmaceutical-grade purity has positioned us among the leading Ivermectin Tablet manufacturers in India serving PAN India and global markets including Africa, the Middle East, and LTAM regions. Our Ivermectin Tablet USP 6mg is produced under stringent quality control systems, ensuring consistent efficacy, safety, and stability across every batch. With advanced manufacturing infrastructure and an experienced technical team, we deliver finished Ivermectin tablets that meet USP standards and global pharmaceutical expectations. Ivermectin Tablets 6mg About Ivermectin Tablet USP 6mg Ivermectin is a widely used antiparasitic medication that plays a critical role in the treatment of parasitic infections affecting the intestinal tract, skin, and eyes. It works by binding to nerve and muscle cells of parasites, leading to paralysis and eventual elimination of the parasites from the body. Our Ivermectin Tablet USP 6mg is carefully formulated to ensure accurate dosage, high bioavailability, and patient compliance, making it suitable […]
Healthcare in Uganda: Overview Uganda’s healthcare system is structured as a pluralistic network of government, private, and not-for-profit facilities delivering services across the country. The Ministry of Health regulates both public and private providers to ensure standards and quality of care. Uganda lacks a comprehensive national health insurance system, and private insurance coverage remains low (approx. 5%). Most healthcare expenditure is funded publicly, with donor support and out-of-pocket spending still significant. Despite progress in expanding access to primary care through Health Centre II, III, and IV levels, health system challenges persist — including uneven distribution of facilities, limited infrastructure outside urban centres, and frequent shortages in essential medical supplies. Main Diseases and Health Challenges Uganda faces a dual burden of disease: communicable diseases still cause high morbidity and mortality, while non-communicable diseases (NCDs) are rising steadily. Communicable Diseases Malaria — one of the leading causes of outpatient attendance and hospital admissions. HIV/AIDS and Tuberculosis (TB) — historically high prevalence, requiring continued public health focus. Ebola Virus Disease — Uganda periodically experiences outbreaks, including recent confirmed cases in Kampala that stressed the healthcare system. Non-Communicable Diseases Hypertension and Diabetes — increasing due to lifestyle changes and urbanization. Neonatal and pediatric conditions […]
Leading Manufacturer and Supplier of Pazopanib Film-Coated Tablets Taj Pharma India stands as a premier manufacturer, exporter, and supplier of Pazopanib film-coated tablets from Vapi, Gujarat, India. Renowned for our commitment to high-quality production, purity, and regulatory compliance, we have established ourselves as a trusted name in the pharmaceutical industry, both nationally and internationally. Our Pazopanib tablets are widely recognized for their efficacy in treating kidney cancer and soft tissue sarcoma, offering patients a reliable solution in oncology therapeutics. What Are Pazopanib Film-Coated Tablets? Pazopanib film-coated Tablets 200mg Pazopanib film-coated tablets are targeted anti-cancer medications that belong to the class of protein kinase inhibitors. These tablets are specifically formulated to inhibit tyrosine kinase enzymes, which play a crucial role in the proliferation of cancer cells. By blocking these enzymes, Pazopanib restricts tumor growth and prevents the formation of new blood vessels that nourish malignant tissues, making it an essential therapy in oncology. Key Features of Pazopanib Tablets: Active Ingredient: Pazopanib Dosage Forms: Film-coated tablets Strengths Available: 200mg (widely used in clinical practice) Indications: Kidney cancer (renal cell carcinoma) and soft tissue sarcoma Mechanism of Action: Inhibits tyrosine kinase receptors, suppresses tumor angiogenesis, and restricts cancer cell growth Why Choose Taj […]
Leading Tirofiban Hydrochloride Injection Manufacturer & Global Supplier Trusted Name in High-Quality Tirofiban Hydrochloride Injection 5mg/100ml We are Taj Pharma India, a well-established Manufacturer, Exporter, and Supplier of Tirofiban Hydrochloride Injection 5mg/100ml based in Vapi, Gujarat, India. With a strong commitment to quality, purity, regulatory compliance, and global healthcare standards, we deliver premium-grade Tirofiban Injection to domestic and international markets including India, Africa, the Middle East, and LTAM regions. Our manufacturing excellence, stringent quality controls, and ethical business practices have positioned us as a leading #1 Tirofiban Hydrochloride Injection Manufacturer & Supplier in India. We assure consistent product quality that meets international pharmacopoeial standards and global regulatory requirements. Tirofiban hydrochloride Injection 5mg/100ml About Tirofiban Hydrochloride Injection Tirofiban Hydrochloride Injection is a potent antiplatelet medication widely used in the management of acute coronary syndromes, including unstable angina and myocardial infarction (heart attack). It plays a critical role in preventing platelet aggregation, thereby reducing the formation of harmful blood clots and improving blood flow to the heart. By inhibiting platelet binding, Tirofiban Injection supports cardiovascular stability and lowers the risk of serious complications such as heart attack or stroke. It is commonly used in hospital and critical care settings under professional supervision. […]
Leading Alendronate Sodium Tablets Manufacturer, Exporter & Supplier in India Trusted Excellence in Alendronate Sodium Tablets Manufacturing We at Taj Pharma India stand as a leading, well-established Manufacturer, Exporter, and Supplier of Alendronate Sodium Tablets in India, delivering unmatched quality, safety, and purity from our advanced manufacturing facilities located in Vapi, Gujarat. With decades of pharmaceutical expertise, we are recognized across PAN India and global markets including Africa, the Middle East, and Latin America (LTAM) as a premium and reliable source for Alendronate Sodium Tablets 70mg and other strengths. Our commitment to stringent quality standards, regulatory compliance, and ethical manufacturing practices makes us the #1 preferred partner for healthcare institutions, distributors, and PCD Pharma Franchise associates seeking consistent, high-efficacy osteoporosis medications. What is Alendronate Sodium and Its Therapeutic Importance Alendronate Sodium Tablets USP 70mg Alendronate Sodium is a clinically proven bisphosphonate widely prescribed for the prevention and treatment of osteoporosis, particularly in postmenopausal women and patients undergoing long-term steroid therapy. It is also used effectively in the management of Paget’s disease of the bone. This medication plays a critical role in bone health management by: Suppressing osteoclast activity, which reduces bone resorption Regulating bone remodeling and turnover Improving bone mineral […]
Leading Manufacturer of Hydralazine Hydrochloride Injection 20mg/ml (Hydrataj) Trusted Name in High-Quality Hydralazine Hydrochloride Injection Manufacturing We at Taj Pharma India take pride in being a well-known and highly trusted manufacturer, exporter, and supplier of Hydralazine Hydrochloride Injection 20mg/ml (Hydrataj). With decades of pharmaceutical excellence, advanced infrastructure, and a strong regulatory-focused approach, we deliver high-quality, high-purity injectable formulations that meet stringent national and international standards. Our Hydralazine Hydrochloride Injection is formulated with precision and manufactured under strict GMP-compliant facilities, ensuring safety, efficacy, and consistency in every batch. This commitment has positioned us as a preferred Hydralazine Hydrochloride Injection manufacturer in India, catering to hospitals, healthcare institutions, government tenders, and pharmaceutical distributors across the globe. What is Hydralazine Hydrochloride Injection? Hydralazine Hydrochloride Injection USP 20mg Hydralazine Hydrochloride Injection belongs to a pharmacological class known as vasodilators. It is primarily indicated for the treatment of severe or life-threatening hypertension, especially in clinical scenarios where oral administration is not feasible or when immediate blood pressure reduction is medically necessary. The injection works by relaxing and widening small blood vessels, enabling smoother blood flow and reducing the workload on the heart. This mechanism makes Hydralazine Hydrochloride Injection a critical drug in emergency and intensive […]
Leading Sorafenib 200mg Tablets Manufacturer, Supplier & Exporter in India Trusted Excellence in Sorafenib Tablets Manufacturing We stand as a well-known Sorafenib 200mg Tablets Manufacturer in India, delivering consistent high-quality, purity, and regulatory-compliant formulations to domestic and international markets. As a trusted Manufacturer, Exporter, and Supplier of Sorafenib Tablets from Vapi, Gujarat, India, we have established a reputation for reliability, precision manufacturing, and ethical pharmaceutical practices. Our Sorafenib Tablets are manufactured under stringent quality controls, ensuring therapeutic effectiveness, safety, and global acceptance. Sorafenib is a proven anti-cancer medication widely prescribed for the treatment of liver cancer, kidney cancer, and thyroid cancer. Our manufacturing expertise, robust infrastructure, and compliance-driven approach make us a preferred Sorafenib Tablets Manufacturer & Supplier PAN India, serving healthcare institutions, distributors, and franchise partners across India, Africa, the Middle East, and LTAM. About Sorafenib Tablets – Mechanism and Therapeutic Value Sorafenib 200mg Tablets Sorafenib Tablets function by blocking the action of abnormal proteins that signal cancer cells to multiply. By inhibiting tumor cell proliferation and angiogenesis, Sorafenib helps stop or slow the spread of cancer cells, supporting effective oncological treatment protocols. This targeted mechanism has positioned Sorafenib as a cornerstone therapy in multiple cancer indications. Our Sorafenib […]
Leading Cytarabine Injection 1gm Manufacturer, Supplier & Exporter in India Trusted #1 Cytarabine Injection 1gm PAN India Manufacturer We are a globally recognized and professionally managed Cytarabine Injection 1gm Manufacturer in India, delivering high-quality oncology injectables with assured purity, safety, and consistency. Under the trusted banner of Taj Pharma, we manufacture, supply, and export Cytarabine Injection 1gm across PAN India and international markets including Africa, Middle East, and LTAM. Our strong manufacturing capabilities, regulatory compliance, and ethical practices position us among the Leading #1 Cytarabine Injection 1gm Manufacturer & Supplier in India, serving hospitals, oncology centers, institutional buyers, distributors, and exporters. Cytarabine Injection 1gm – High-Purity Oncology Formulation Cytarabine Injection USP 1gm Cytarabine Injection 1gm is a potent anticancer injectable widely used in the treatment of blood cancers, including leukemia. The formulation works by interfering with DNA and RNA synthesis in cancer cells, preventing their growth and multiplication. Manufactured under strictly controlled sterile conditions, our Cytarabine Injection ensures optimal therapeutic performance and patient safety. Each unit of Cytarabine Injection 1gm – Taj Pharma undergoes rigorous quality testing to ensure batch consistency, stability, and compliance with global pharmaceutical standards. Well-Established Cytarabine Injection 1gm Manufacturer from Vapi, Gujarat Taj Pharma operates advanced […]
Leading Cytarabine Injection BP 2gm Manufacturer, Supplier & Exporter in India Trusted #1 Cytarabine Injection BP 2gm PAN India Manufacturer We are a globally trusted and well-established Cytarabine Injection BP 2gm manufacturer in India, delivering premium-quality oncology injectables that meet stringent national and international pharmaceutical standards. Under the strong brand presence of Taj Pharma, we manufacture, supply, and export Cytarabine Injection BP 2gm across PAN India and international markets including Africa, the Middle East, and LTAM regions. Our commitment to quality, purity, and compliance has positioned us as a Leading #1 Cytarabine Injection BP 2gm Manufacturer & Supplier in India, trusted by hospitals, oncology centers, government institutions, and pharmaceutical distributors. Cytarabine Injection BP 2gm – High-Purity Oncology Injectable Cytarabine Injection BP 2gm Cytarabine Injection BP 2gm is a potent antineoplastic medicine widely used in the treatment of blood cancers, including leukemia. Manufactured using advanced sterile technology, Cytarabine works by interfering with the DNA and RNA synthesis of cancer cells, effectively preventing their growth and multiplication. Each vial of Cytarabine Injection BP 2gm – Taj Pharma is produced with strict quality assurance protocols to ensure safety, stability, and consistent therapeutic efficacy. Well-Established Cytarabine Injection BP 2gm Manufacturer from Vapi, Gujarat Taj […]
Leading Cytarabine Injection BP 500mg Manufacturer, Supplier & Exporter in India We stand as a trusted name in the Indian pharmaceutical industry as Taj Pharma, a globally recognized Cytarabine Injection BP 500mg Manufacturer, Supplier, and Exporter. With advanced manufacturing facilities in Vapi, Gujarat, India, we deliver high-quality, high-purity Cytarabine Injection BP 500mg that complies with stringent international quality standards. Our commitment to quality, consistency, and patient safety has positioned us as a #1 Cytarabine Injection Manufacturer PAN India and a preferred exporter to Africa, the Middle East, LATAM, and other global markets. About Cytarabine Injection BP 500mg Cytarabine Injection BP 500mg is a widely used chemotherapy medication primarily indicated for the treatment of blood cancers, including various forms of leukemia. Cytarabine works by interfering with DNA and RNA synthesis in rapidly dividing cancer cells. By substituting essential building blocks of genetic material, it inhibits cancer cell growth and multiplication, thereby helping control the progression of malignancy. Administered intravenously via a drip, Cytarabine Injection BP 500mg is used strictly under medical supervision, ensuring accurate dosing and patient monitoring during therapy. Why We Are the Best Cytarabine Injection BP 500mg Manufacturer in India Cytarabine Injection BP 500mg As a leading Cytarabine Injection […]
Leading Azacitidine for Injection 100mg Manufacturer, Supplier & Exporter in India We stand as a trusted and globally recognized manufacturer, exporter, and supplier of Azacitidine for Injection 100mg in India, delivering unmatched quality, purity, and compliance with international pharmaceutical standards. Taj Pharma India, headquartered in Vapi, Gujarat, has established itself as a benchmark name in oncology injectable manufacturing, serving domestic and international markets with reliability and excellence. Our expertise, advanced infrastructure, and stringent quality systems enable us to consistently deliver premium-grade Azacitidine 100mg Injection for the treatment of complex hematological malignancies, including Myelodysplastic Syndrome (MDS) and specific forms of blood cancer (leukemia). Azacitidine for Injection 100mg – High-Purity Oncology Solution Azacitidine for Injection 1 vial/20ml Azacitidine for Injection 100mg is a potent anticancer medication classified as a hypomethylating agent. It works by interfering with DNA and RNA synthesis, thereby inhibiting the growth of malignant cells and promoting normal maturation of blood cells within the bone marrow. We manufacture Azacitidine Injection 100mg using validated processes that ensure: High chemical purity Optimal stability Accurate potency Low impurity profiles Strict sterility assurance Our formulations are designed to meet global regulatory expectations, making them suitable for hospital supply, oncology centers, government tenders, and export […]
Leading Human Coagulation Factor VIII 500IU Manufacturer, Supplier & Exporter in India Trusted Excellence in Human Coagulation Factor VIII 500IU Manufacturing We are Taj Pharma India, a globally trusted Manufacturer, Exporter, and Supplier of Human Coagulation Factor VIII 500IU, headquartered in Vapi, Gujarat, India. With decades of pharmaceutical expertise, robust infrastructure, and strict adherence to international quality standards, we deliver high-purity, high-efficacy Human Coagulation Factor VIII 500IU that meets the critical needs of patients suffering from Hemophilia A and bleeding disorders. Our commitment to quality assurance, product purity, safety, and therapeutic reliability has positioned us as a leading #1 Human Coagulation Factor VIII 500IU Manufacturer & Supplier in India, catering to PAN India markets, Africa, the Middle East, LATAM, and other regulated and semi-regulated global regions. What Is Human Coagulation Factor VIII 500IU? Human Coagulation Factor viii 500IU Human Coagulation Factor VIII is a vital blood-clotting protein required to prevent and control bleeding. Patients with Hemophilia A lack or have insufficient Factor VIII, resulting in prolonged or spontaneous bleeding episodes. Our Human Coagulation Factor VIII 500IU formulation helps: Restore clotting ability Prevent internal and external bleeding Reduce bleeding frequency Improve patient quality of life We manufacture this life-saving product under […]
Leading Cytarabine Injection BP 100mg Manufacturer, Supplier & Exporter in India Trusted Excellence in Cytarabine Injection BP 100mg Manufacturing We stand at the forefront of pharmaceutical manufacturing as Taj Pharma, a globally recognized and trusted Cytarabine Injection BP 100mg Manufacturer in India. With a strong foundation built on quality, compliance, and innovation, we deliver high-purity Cytarabine Injection BP 100mg that meets stringent international pharmacopoeial standards. Our commitment extends across PAN India manufacturing, reliable supply chains, and a robust export network spanning Africa, the Middle East, LTAM, and other regulated and semi-regulated markets. Our manufacturing operations are anchored in Vapi, Gujarat, one of India’s most prominent pharmaceutical hubs, enabling us to ensure consistent quality, scalability, and on-time delivery for hospitals, oncology centers, government tenders, distributors, and PCD Pharma Franchise partners. Cytarabine Injection BP 100mg: Therapeutic Significance Cytarabine Injection BP 100mg Cytarabine Injection BP 100mg is a critical antineoplastic agent widely used in the treatment of blood cancers, including acute leukemias. Cytarabine functions by interfering with DNA and RNA synthesis in rapidly dividing cancer cells. By substituting essential building blocks of nucleic acids, it effectively prevents cancer cell growth and multiplication, supporting oncological treatment protocols globally. Administered intravenously via infusion, Cytarabine Injection […]
Leading Manufacturer, Exporter, and Supplier of Tirofiban Hydrochloride I.V. Injection 5mg/100ml Trusted Tirofiban Hydrochloride I.V. Injection Manufacturer in India We are Taj Pharma India, a well-established, globally recognized Manufacturer, Exporter, and Supplier of Tirofiban Hydrochloride I.V. Injection 5mg/100ml based in Vapi, Gujarat, India. With decades of pharmaceutical expertise, advanced manufacturing infrastructure, and uncompromising quality standards, we deliver high-purity, safe, and effective antiplatelet injections trusted by hospitals, cardiologists, and healthcare institutions across India, Africa, the Middle East, and LTAM regions. Our Tirofiban Hydrochloride I.V. Injection is manufactured under stringent WHO-GMP compliant facilities, ensuring consistent quality, sterility, and therapeutic efficacy. We are committed to providing premium injectable formulations that meet both domestic and international regulatory requirements. About Tirofiban Hydrochloride I.V. Injection 5mg/100ml Tirofiban Hydrochloride I.V. Injection 5mg/100ml Tirofiban Hydrochloride I.V. Injection is a potent antiplatelet medication widely used in the management of acute coronary syndromes, including unstable angina and heart attack (myocardial infarction). It plays a crucial role in preventing platelet aggregation, thereby reducing the formation of dangerous blood clots that can obstruct coronary arteries. Our Tirofiban Injection 5mg/100ml is formulated for intravenous administration, offering rapid onset of action and precise dosing in critical cardiac care settings. Mechanism of Action We manufacture […]
Leading Deferiprone Capsules 250mg Manufacturer in India We are recognized as a Leading #1 Deferiprone Capsules 250mg Manufacturer & Supplier in India, offering pharmaceutical products that meet the highest standards of quality, purity, and safety. With a strong manufacturing base in Vapi, Gujarat, we deliver Deferiprone Capsules 250mg across PAN India and to multiple international markets. Our commitment to excellence, regulatory compliance, and patient-centric manufacturing has positioned us as a trusted name in iron chelation therapy. Deferiprone Capsules 250mg – High-Purity Iron Chelation Therapy Deferiprone Capsules 250mg Deferiprone Capsules 250mg are widely prescribed for the treatment of iron overload, especially in patients suffering from transfusion-dependent thalassemia. Excess iron accumulation can cause serious damage to vital organs such as the heart and liver. Our formulation works by trapping excess iron and facilitating its removal, primarily through the stools, thereby reducing the long-term risk of organ damage. Each capsule is manufactured using high-quality active pharmaceutical ingredients (API) and advanced formulation techniques to ensure consistent bioavailability and therapeutic effectiveness. Well-Established Manufacturer, Exporter & Supplier from Vapi, Gujarat As a well-established Manufacturer, Exporter, and Supplier of Deferiprone Capsules 250mg from Vapi, Gujarat, we operate state-of-the-art manufacturing facilities compliant with GMP and international quality standards. […]
Leading Deferiprone Capsules 500mg Manufacturer, Exporter & Supplier in India Trusted Assurance of Quality, Purity, and Global Compliance We stand as a globally trusted name in pharmaceutical manufacturing, delivering Deferiprone Capsules 500mg with uncompromising quality, purity, and regulatory compliance. As a well-established Manufacturer, Exporter, and Supplier from Vapi, Gujarat, India, we ensure that every capsule reflects our commitment to patient safety, therapeutic efficacy, and international standards. Our Deferiprone Capsules 500mg are widely recognized for their role in the management of iron overload, particularly in patients suffering from transfusion-dependent thalassemia. Through stringent quality control systems, advanced manufacturing infrastructure, and an experienced scientific team, we consistently deliver pharmaceutical products that meet WHO-GMP, ISO, and international export norms. Deferiprone Capsules 500mg: Effective Iron Chelation Therapy Deferiprone Capsules 500mg Deferiprone is an orally active iron chelator designed to bind excess iron in the body and facilitate its elimination primarily through the stools. This mechanism significantly reduces the risk of iron-induced organ damage, including complications affecting the heart, liver, and endocrine organs. Key Therapeutic Benefits Reduces iron overload caused by repeated blood transfusions Improves long-term survival in thalassemia patients Prevents cardiac and hepatic complications Oral administration for patient convenience Clinically proven efficacy and safety profile […]
Leading Oxaliplatin Injection 100mg Manufacturer, Supplier & Exporter in India Trusted Oxaliplatin Injection 100mg Manufacturer in India We at Taj Pharma India take pride in being a well-established, reliable, and globally trusted manufacturer, exporter, and supplier of Oxaliplatin Injection 100mg. Based in Vapi, Gujarat, India, our manufacturing facilities are designed to meet international pharmaceutical quality standards, ensuring unmatched purity, safety, and therapeutic effectiveness. As a PAN India Oxaliplatin Injection Manufacturer, we cater to hospitals, oncology centers, government tenders, distributors, wholesalers, and PCD Pharma Franchise partners across India, Africa, the Middle East, LTAM, and other global markets. Our commitment to quality, regulatory compliance, and ethical business practices has positioned us as a leading #1 Oxaliplatin Injection 100mg Manufacturer & Supplier in India. About Oxaliplatin Injection 100mg Oxaliplatin Injection USP 100mg/Vial Oxaliplatin Injection 100mg is a widely prescribed anti-cancer (anticancer / antineoplastic) medication, primarily used in the treatment of colon cancer and rectal cancer. It belongs to the platinum-based chemotherapy drug class and is commonly used in combination therapy protocols as recommended by oncologists. Mechanism of Action Oxaliplatin works by damaging the genetic material (DNA and RNA) of cancer cells. This action stops or slows down the growth and multiplication of malignant […]
Leading Carboplatin Injection 450mg/45ml Manufacturer, Exporter, and Supplier in India Trusted Manufacturer of High-Purity Carboplatin Injection 450mg/45ml We are a globally recognized manufacturer, exporter, and supplier of Carboplatin Injection 450mg/45ml, delivering uncompromised quality, safety, and therapeutic efficacy. Taj Pharma India, headquartered in Vapi, Gujarat, stands as a benchmark for pharmaceutical excellence, offering WHO-GMP compliant oncology injectables to domestic and international markets. Our Carboplatin Injection 450mg/45ml is manufactured under stringent quality systems to ensure high purity, stability, and consistent clinical performance. Carboplatin Injection 450mg/45ml – Oncology Therapeutic Excellence Carboplatin Injection 450mg/45ml is a platinum-based anti-cancer medication widely prescribed in the treatment of ovarian cancer and small cell lung cancer. The formulation works by damaging the genetic material (DNA and RNA) of cancer cells, effectively stopping or slowing down cancer cell growth and multiplication. Our manufacturing process prioritizes precise dosage accuracy, sterile conditions, and validated formulations to meet the critical needs of oncology care. Why Taj Pharma is the #1 Carboplatin Injection Manufacturer in India Carboplatin Injection 450mg/45ml Unmatched Quality Assurance We follow international quality standards, including GMP, ISO, and rigorous in-house quality control protocols. Each batch of Carboplatin Injection 450mg/45ml undergoes comprehensive analytical testing, ensuring potency, sterility, and safety before release. […]
WHO–GMP | PIC/S (Thailand) | Global Export & Collaboration Partner Taj Pharma India Ltd. is a globally trusted pharmaceutical manufacturer offering a comprehensive range of dermatological, topical, ophthalmic, antiseptic, antifungal, antibacterial, anti-inflammatory, cosmetic and specialty external preparations. Manufactured at our WHO‑GMP compliant facilities with PIC/S (Thailand) approval, our products are designed to meet stringent international quality, safety, and regulatory expectations. We actively invite collaboration, private label partnerships, contract manufacturing (CMO/CDMO), technology transfer, and dossier-based exports for regulated and semi‑regulated markets. With major regulatory inspections scheduled next year from Africa, ASEAN countries, and the MENA region, Taj Pharma continues to strengthen its global compliance footprint. Why Partner with Taj Pharma? WHO‑GMP & PIC/S (Thailand) approved manufacturing Broad external formulations: Ointments, Creams, Gels, Lotions, Shampoos, Powders, Solutions, Dental & Eye Preparations Ready formulations adaptable to local pharmacopeias & market needs Private label & country‑specific branding support Export experience across Africa, ASEAN, CIS & MENA regions Strong QA/QC, stability studies & regulatory documentation support External Preparations – Master Product Table Sr. No.Generic NameStrengthPack SizeDosage Form / Section1Aciclovir5%10 gmOintment2Beclomethasone Dipropionate + Clotrimazole0.025% + 1%15 gmOintment3Beclomethasone Dipropionate + Clotrimazole + Neomycin Sulphate0.025% + 1% + 0.5%10 gmOintment4Choline Salicylate + Lidocaine HCl8.7% + 2%5 gmGel5Clindamycin + […]
Premier Manufacturer of Deferasirox Dispersible Tablets 400mg Taj Pharma India has firmly established itself as a leading manufacturer, exporter, and supplier of Deferasirox Dispersible Tablets 400mg in India. With state-of-the-art facilities located in Vapi, Gujarat, Taj Pharma consistently delivers high-quality and pharma-grade medications that meet rigorous domestic and international standards. Our commitment to excellence ensures that healthcare providers and patients receive safe, reliable, and effective iron chelation therapy for managing chronic iron overload. Understanding Deferasirox Dispersible Tablets 400mg Deferasirox Dispersible Tablets 400mg Deferasirox Tablets are a specialized iron chelation therapy designed to treat chronic iron overload, particularly in patients with transfusion-dependent or non-transfusion-dependent thalassemia syndromes. The medication works by binding excess iron in the bloodstream, forming a complex that is excreted naturally through fecal elimination, helping to prevent organ damage caused by iron accumulation. Key Benefits of Deferasirox Dispersible Tablets 400mg: Efficiently reduces excess iron levels in the body. Non-invasive oral therapy, eliminating the need for injections. Suitable for both transfusion-dependent and non-transfusion-dependent patients. Manufactured under strict GMP and WHO guidelines ensuring purity and consistency. Why Choose Taj Pharma India for Deferasirox Dispersible Tablets? Deferasirox Dispersible Tablets 400mg As a trusted name in the pharmaceutical industry, Taj Pharma India is […]
Leading Deferasirox Dispersible Tablets 100mg Manufacturer, Exporter & Supplier in India Trusted Name for High-Quality Deferasirox Dispersible Tablets 100mg We at Taj Pharma India are proud to be a well-known, trusted, and globally recognized manufacturer, exporter, and supplier of Deferasirox Dispersible Tablets 100mg from Vapi, Gujarat, India. With a strong commitment to quality, purity, safety, and regulatory compliance, we deliver premium-grade Deferasirox Tablets that meet international pharmaceutical standards and global healthcare expectations. Our Deferasirox Dispersible Tablets are widely supplied PAN India and exported to Africa, the Middle East, LTAM regions, and other global markets, making us a preferred choice among healthcare providers, distributors, and pharmaceutical partners worldwide. About Deferasirox Dispersible Tablets 100mg Deferasirox Dispersible Tablets 100mg Deferasirox Tablets are a clinically proven oral iron chelator used to manage chronic iron overload in patients suffering from conditions such as transfusion-dependent and non-transfusion-dependent thalassemia syndromes. Excess iron accumulation due to repeated blood transfusions can cause severe organ damage, and Deferasirox plays a vital role in binding excess iron and facilitating its elimination from the body. Deferasirox Dispersible Tablets 100mg work by forming a stable complex with iron, which is then excreted through the stool, helping to maintain healthy iron levels in the […]
Leading Etoricoxib Tablets 90mg (Rezoxib) Manufacturer, Exporter, and Supplier in India Trusted Manufacturer of High-Quality Etoricoxib Tablets 90mg (Rezoxib) We are Taj Pharma India, a well-established and highly reputed Manufacturer, Exporter, Distributor, and Supplier of Etoricoxib Tablets 90mg (Rezoxib) from Vapi, Gujarat, India. With decades of pharmaceutical excellence, we deliver international-standard, high-purity, and quality-assured Etoricoxib Tablets that meet stringent regulatory and quality benchmarks. Our manufacturing strength, scientific expertise, and customer-centric approach have positioned us as a leading Etoricoxib Tablets Manufacturer PAN India and a premium exporter to Africa, the Middle East, and LTAM regions. About Etoricoxib Tablets 90mg (Rezoxib) Etoricoxib Tablets 90mg Etoricoxib is a non-steroidal anti-inflammatory drug (NSAID) belonging to the COX-2 inhibitor class. Etoricoxib Tablets 90mg are widely prescribed for pain relief and inflammation management in conditions such as: Rheumatoid arthritis Osteoarthritis Ankylosing spondylitis Acute musculoskeletal pain Chronic inflammatory disorders By selectively inhibiting COX-2 enzymes, Etoricoxib Tablets help reduce pain, swelling, and stiffness, offering effective symptomatic relief with fewer gastric side effects compared to traditional NSAIDs like ibuprofen or naproxen. Why Taj Pharma India is the #1 Etoricoxib Tablets Manufacturer in India Etoricoxib Tablets 90mg World-Class Manufacturing Infrastructure We operate WHO-GMP compliant manufacturing facilities in Vapi, Gujarat, equipped […]
Leading Methotrexate Injection 1000mg/40ml Manufacturer, Exporter & Supplier in India Trusted Name in High-Quality Methotrexate Injection Manufacturing We at Taj Pharma India stand as a well-known and trusted Manufacturer, Exporter, Distributor, and Supplier of Methotrexate Injection 1000mg/40ml from Vapi, Gujarat, India. With years of pharmaceutical manufacturing excellence, we assure high-quality, purity, safety, and regulatory compliance in every batch of Methotrexate Injection we produce. Our expertise, state-of-the-art infrastructure, and stringent quality control systems position us among the leading Methotrexate Injection manufacturers PAN India, serving both domestic and international pharmaceutical markets with consistency and reliability. About Methotrexate Injection 1000mg/40ml Methotrexate Injection 1000mg/40ml Methotrexate Injection is a widely prescribed immunosuppressant and antimetabolite medication used in the treatment of rheumatoid arthritis, psoriasis, and other autoimmune disorders. It works by reducing immune system activity, helping to control inflammation, swelling, pain, and abnormal skin cell growth. As a finished Methotrexate Injection manufacturer in India, we ensure pharmaceutical-grade formulation with optimal efficacy and safety. Therapeutic Uses of Methotrexate Injection Methotrexate Injection 1000mg/40ml Methotrexate Injection is clinically effective in: Rheumatoid Arthritis – Reduces inflammation, pain, joint stiffness, and improves physical function Psoriasis – Slows down excessive skin cell production and reduces skin lesions Autoimmune conditions requiring immune system […]
Leading Fenbendazole Tablets 222mg Manufacturer in India with Assured Quality & Purity Trusted Manufacturer of Fenbendazole Tablets 222mg (Orray) in India We at Taj Pharma India stand as a leading and trusted Manufacturer, Exporter, and Supplier of Fenbendazole Tablets 222mg (Orray) from Vapi, Gujarat, India. With decades of pharmaceutical manufacturing excellence, we deliver high-quality, pure, and reliable Fenbendazole formulations that meet stringent international quality standards. Our commitment to innovation, regulatory compliance, and customer satisfaction has positioned us among the top Fenbendazole Tablets 222mg manufacturers in India with a strong footprint across PAN India, Africa, the Middle East, and LTAM markets. Fenbendazole Tablets 222mg (Orray) – Premium Anthelmintic Formulation Fenbendazole Tablets 222mg Fenbendazole Tablets 222mg (Orray) are a broad-spectrum anthelmintic formulation widely used for the treatment of parasitic worm infections. Manufactured under GMP-certified facilities, our tablets are formulated to ensure consistent potency, bioavailability, and stability. Fenbendazole is widely prescribed to treat parasitic infections such as: Roundworms Hookworms Whipworms Tapeworms Protozoal infections like Giardia It works by disrupting the cellular microtubule structure of parasites, thereby inhibiting glucose uptake and leading to parasite death. Well-Established Fenbendazole Tablets Manufacturer from Vapi, Gujarat Fenbendazole Tablets 222mg As a well-established Fenbendazole Tablets 222mg manufacturer from Vapi, […]
Leading Fenbendazole Tablets 444mg (Orray) Manufacturer in India with Assured Quality and Purity We are a globally trusted pharmaceutical organization recognized for manufacturing and supplying Fenbendazole Tablets 444mg (Orray) that meet the highest standards of quality, purity, safety, and consistency. As a well-established Manufacturer, Exporter, and Supplier from Vapi, Gujarat, India, we deliver premium-grade Fenbendazole formulations across PAN India, Africa, the Middle East, and LTAM markets. Our commitment to GMP-compliant manufacturing, stringent quality control systems, and regulatory-aligned processes positions us among the Leading #1 Fenbendazole Tablets 444mg Manufacturers & Suppliers in India. Every batch is produced with precision to ensure reliable therapeutic performance and long-term stability. Fenbendazole Tablets 444mg (Orray): High-Purity Anthelmintic Formulation Fenbendazole Tablets 444mg (Orray) are formulated as a broad-spectrum anthelmintic (dewormer) primarily used in veterinary medicine to treat a wide range of parasitic worm infections. The formulation is known for its targeted action, dependable absorption profile, and controlled potency. Fenbendazole functions by disrupting the cellular structure of parasites, inhibiting glucose uptake and microtubule formation, leading to parasite elimination. This mechanism ensures effective results against multiple parasites with a well-tolerated safety profile when used as prescribed. Therapeutic Applications of Fenbendazole Tablets 444mg Fenbendazole Tablets 444mg Our Fenbendazole Tablets […]
Leading Manufacturer of Phenoxymethylpenicillin Potassium Tablets (Penitaj-V) with Assured Quality and Purity Trusted Phenoxymethylpenicillin Potassium Manufacturer in India We stand as a well-established and globally recognized manufacturer, exporter, and supplier of Phenoxymethylpenicillin Potassium Tablets (Penitaj-V) from Vapi, Gujarat, India. With decades of pharmaceutical excellence, we deliver high-quality, pure, and reliable antibiotic formulations that comply with stringent international quality standards. Our commitment to precision manufacturing, validated processes, and regulatory compliance has positioned us as a preferred Phenoxymethylpenicillin Potassium supplier across PAN India, Africa, the Middle East, and LTAM markets. Phenoxymethylpenicillin Potassium is a penicillin-class antibiotic widely prescribed to treat bacterial infections of the throat, ear, nasal sinuses, respiratory tract, skin, and soft tissues. It is also indicated in the management of sexually transmitted infections such as syphilis and in the prevention of rheumatic fever. Our Penitaj-V Tablets are formulated to deliver consistent therapeutic efficacy, rapid bacterial growth inhibition, and dependable patient outcomes. About Phenoxymethylpenicillin Potassium (Penitaj-V) Phenoxymethylpenicillin Tablets BP 1,000,000 I.U. Phenoxymethylpenicillin Potassium works by stopping the growth of gram-positive bacteria, thereby controlling and eliminating infection at the source. As a time-tested antibiotic, it remains a cornerstone in clinical practice when used responsibly and as prescribed. Key therapeutic applications include: Throat […]
Leading Manufacturer and Supplier of Phenoxymethylpenicillin Tablets BP 250mg Taj Pharma India stands as a premier Manufacturer, Exporter, and Supplier of Phenoxymethylpenicillin Tablets BP 250mg in India. With a commitment to delivering high-quality, pure, and effective antibiotics, we cater to healthcare providers and distributors across India, Africa, the Middle East, and LATAM regions. Our flagship product, PHENI-V 250mg, is a trusted solution for a wide range of bacterial infections, offering patients a reliable and potent antibiotic therapy. High-Quality Phenoxymethylpenicillin Tablets 250mg Phenoxymethylpenicillin Tablets BP 250mg Phenoxymethylpenicillin, commonly referred to as penicillin V, is a broad-spectrum antibiotic primarily used to treat bacterial infections such as: Throat infections, including streptococcal pharyngitis Ear infections Nasal sinus infections Respiratory tract infections, including bronchitis and pneumonia Skin and soft tissue infections Sexually transmitted infections, including syphilis In addition to treatment, PHENI-V 250mg is frequently prescribed for the prevention of rheumatic fever, providing a critical role in long-term health management. At Taj Pharma India, we ensure that every tablet meets stringent quality control measures to maintain the highest standard of purity and potency, making our products safe and effective for global distribution. Trusted Manufacturing and Supply in India Phenoxymethylpenicillin Tablets BP 250mg Based in Vapi, Gujarat, […]
Trusted Manufacturer of Phenoxymethylpenicillin Tablets BP 500mg in India Leading Excellence in Phenoxymethylpenicillin Tablets Manufacturing We are recognized as a leading manufacturer, exporter, distributor, and supplier of Phenoxymethylpenicillin Tablets BP 500mg (PHENI-V) in India. Operating from Vapi, Gujarat, our advanced pharmaceutical manufacturing infrastructure ensures consistent quality, high purity, and global regulatory compliance. Our commitment to excellence has positioned us as a preferred partner for domestic and international markets, including Africa, the Middle East, LTAM, and PAN India distribution networks. Phenoxymethylpenicillin Tablets are a trusted penicillin-class antibiotic widely prescribed for the treatment and prevention of bacterial infections. With stringent quality assurance protocols and world-class manufacturing practices, we deliver formulations that meet BP standards and exceed customer expectations. About Phenoxymethylpenicillin Tablets BP 500mg (PHENI-V) Phenoxymethylpenicillin Tablets BP 500mg Phenoxymethylpenicillin, also known as Penicillin V, is an antibiotic that effectively kills gram-positive bacteria by inhibiting the formation of the bacterial cell wall. This mechanism prevents bacterial survival and replication, making it a reliable treatment option for various infections. PHENI-V 500mg Tablets are manufactured to provide: High bioavailability Accurate dosage consistency Excellent stability and shelf life Optimal therapeutic efficacy Our tablets are designed for oral administration on an empty stomach, ensuring maximum absorption and […]
Leading Bezafibrate Tablet 400mg (Bezotaj) Manufacturer, Supplier & Exporter in India Trusted Manufacturer of Bezafibrate Tablet 400mg (Bezotaj) with Assured Quality & Purity We are Taj Pharmaceuticals Ltd, a well-established and globally trusted manufacturer, exporter, distributor, and supplier of Bezafibrate Tablet 400mg (Bezotaj) from Vapi, Gujarat, India. With decades of pharmaceutical excellence, advanced manufacturing infrastructure, and strict quality assurance systems, we deliver high-quality Bezafibrate tablets that meet international regulatory standards and therapeutic expectations across domestic and global markets. As a leading Bezafibrate Tablet manufacturer PAN India, we ensure every batch reflects consistency, purity, safety, and efficacy, making us the preferred partner for healthcare institutions, wholesalers, exporters, and PCD pharma franchise associates. Bezafibrate Tablet 400mg (Bezotaj) – Product Overview Bezafibrate 400mg tablet Bezafibrate Tablet 400mg, marketed under the brand Bezotaj, is a lipid-lowering medication primarily used in the management of high cholesterol and elevated triglyceride levels. It plays a critical role in reducing cardiovascular risks when combined with lifestyle modifications such as regular exercise and a low-fat diet. Therapeutic Benefits of Bezafibrate Tablet Reduces triglyceride levels Lowers LDL (bad cholesterol) Increases HDL (good cholesterol) Helps prevent heart disease Reduces the risk of stroke and heart attack Our Bezafibrate Tablet 400mg (Bezotaj) […]
Leading Manufacturer and Supplier of Levetiracetam Tablets 250mg (Leepra XR) Taj Pharma India has established itself as a premier manufacturer, exporter, and supplier of high-quality Levetiracetam Tablets 250mg (Leepra XR) in India. Based in Vapi, Gujarat, we are committed to delivering products of unmatched purity, efficacy, and safety to clients across India, Africa, the Middle East, and LATAM. Our dedication to quality ensures that our clients receive reliable anticonvulsant medications essential for the treatment of epilepsy and seizures. High-Quality Levetiracetam Tablets 250mg Manufacturing Standards Levetiracetam Tablets 250mg At Taj Pharma India, every batch of Levetiracetam Tablets undergoes rigorous quality control procedures. Our state-of-the-art manufacturing facilities in Vapi, Gujarat, comply with WHO-GMP standards, ensuring that each tablet maintains high purity and potency. Levetiracetam is an antiepileptic drug that binds to SV2A receptors on nerve cell surfaces, preventing the spread of abnormal electrical signals in the brain that cause seizures. This mechanism makes Levetiracetam Tablets highly effective in controlling partial-onset seizures, myoclonic seizures, and generalized tonic-clonic seizures. Reliable Supply Across PAN India and International Markets Taj Pharma India is not only a top manufacturer but also a trusted exporter and supplier of Levetiracetam Tablets 250mg across India, Africa, the Middle East, and […]
Leading Abacavir Tablets USP 300mg Manufacturer, Supplier, and Exporter Trusted Manufacturer of Abacavir Tablets USP 300mg in India We are Taj Pharma India, a well-established and globally recognized manufacturer, exporter, and supplier of Abacavir Tablets USP 300mg based in Vapi, Gujarat, India. With decades of pharmaceutical manufacturing expertise, we deliver high-quality, high-purity Abacavir Tablets that meet stringent USP, WHO-GMP, and international regulatory standards. Our commitment to quality assurance, consistent supply, and ethical pharmaceutical practices has positioned us as a leading Abacavir Tablets manufacturer in India serving domestic and international markets. Abacavir Tablets USP 300mg are an essential antiviral medication widely prescribed in the management of HIV infection and chronic Hepatitis B virus (HBV) infection. As a premium Abacavir Tablets exporter, we serve clients across PAN India, Africa, the Middle East, LTAM, and other regulated and semi-regulated markets. Why Taj Pharma India is the Preferred Abacavir Tablets Manufacturer Abacavir Tablets USP 300mg We distinguish ourselves as a trusted Abacavir Tablets USP 300mg manufacturer and supplier by maintaining the highest benchmarks in manufacturing precision, product safety, and regulatory compliance. Key Strengths of Taj Pharma India WHO-GMP & ISO Certified Manufacturing Facility USP-grade Active Pharmaceutical Ingredients (API) Strict Quality Control & Batch-to-Batch Consistency […]
A Leading Levetiracetam Tablets 500mg (Leepra XR) Manufacturer in India We stand as a trusted, well-established, and globally recognized manufacturer, exporter, and supplier of Levetiracetam Tablets 500mg (Leepra XR) from Vapi, Gujarat, India. Our commitment to quality, purity, regulatory compliance, and patient safety positions us among the top Levetiracetam Tablets manufacturers in India, serving domestic and international markets with excellence. Levetiracetam Tablets are widely prescribed in the treatment of epilepsy and seizure disorders, and we ensure every batch meets stringent pharmaceutical quality standards. With advanced manufacturing infrastructure and experienced professionals, we consistently deliver premium-grade antiepileptic formulations to healthcare providers, distributors, and partners across India, Africa, the Middle East, and LTAM regions. Why Taj Pharma India Is the Preferred Levetiracetam Tablets Manufacturer Levetiracetam tablets 500mg We differentiate ourselves through precision manufacturing, ethical practices, and supply reliability. As a PAN India Levetiracetam Tablets 500mg (Leepra XR) manufacturer, we focus on delivering consistent therapeutic performance supported by strict quality control systems. Key strengths include: WHO-GMP compliant manufacturing facilities High-purity active pharmaceutical ingredients Validated production and packaging processes Robust quality assurance and quality control Efficient logistics and export documentation Competitive pricing with assured batch consistency Our presence as a Levetiracetam Tablets manufacturer in Vapi, […]
Leading Manufacturer of Udenafil Tablets 100mg (Zyogra) in India Trusted Name for High-Quality Udenafil Tablets Manufacturing & Export We are Taj Pharma India, a well-known Manufacturer, Exporter, Distributor, and Supplier of Udenafil Tablets 100mg (Zyogra) based in Vapi, Gujarat, India. Our organization is recognized across PAN India and international markets for delivering high-quality, pure, and effective Udenafil Tablets that meet stringent pharmaceutical standards. With years of expertise, advanced infrastructure, and strict quality control systems, we ensure that every tablet manufactured by us delivers consistent efficacy, safety, and reliability. Our Udenafil Tablets 100mg (Zyogra) are widely supplied across India, Africa, the Middle East, LTAM, and other global markets, making us a preferred premium manufacturer and exporter. About Udenafil Tablets 100mg (Zyogra) Udenafil Tablet 100mg Udenafil is a clinically proven phosphodiesterase type-5 (PDE-5) inhibitor used primarily in the treatment of: Erectile Dysfunction (ED) Pulmonary Arterial Hypertension (PAH) Benign Prostatic Hyperplasia (BPH) Udenafil works by increasing blood flow to specific areas of the body. In erectile dysfunction, it relaxes the smooth muscles of penile blood vessels, allowing enhanced blood flow and helping achieve and maintain an erection only when sexual stimulation is present. Our Udenafil Tablets 100mg (Zyogra) are formulated to offer rapid […]
Oral Rehydration Salt (ORS) is a life-saving formulation recommended by the WHO and Ministry of Health for the prevention and treatment of dehydration caused by diarrhoea, heat exposure, vomiting, and intense physical activity. As one of India’s Top 10 Generic Drug Manufacturers, Taj Pharma India has become a leading name in supplying high-quality, affordable ORS powders to both domestic and international markets. With state-of-the-art GMP/WHO-cGMP manufacturing facilities at, Vapi (Gujarat) and a strong R&D foundation, Taj Pharma ensures reliability, consistency, and global compliance in every batch of ORS produced. Wide Range of Flavours for Every Age Group Taj Pharma offers premium, refreshing, and consumer-friendly ORS flavours, ideal for children, adults, and elderly patients: Orange Flavour ORS Powder Lemon Flavour ORS Powder Mango Flavour ORS Powder Pineapple Flavour ORS Powder Plain / WHO Formula ORS Powder Custom flavours available on demand Each formulation is designed for excellent taste, fast dissolution, and high patient compliance. Affordability Without Compromise In alignment with Taj Pharma’s mission to provide quality healthcare at affordable prices, ORS is manufactured using optimized processes, bulk sourcing, and efficient QA/QC systems. This ensures: Competitive pricing for government tenders Bulk supply rates for schools, NGOs, hospitals, and export markets Cost-effective private […]
Leading Pentoxifylline 400mg Tablets Manufacturer, Supplier & Exporter in India As a globally recognized pharmaceutical company, Taj Pharma stands at the forefront of manufacturing Pentoxifylline 400mg Tablets with unmatched quality, purity, and regulatory compliance. With a state-of-the-art facility in Vapi, Gujarat, India, we are committed to delivering world-class formulations across India, Africa, the Middle East, LATAM, and emerging global markets. Our reputation as a top Pharmaceutical Manufacturer, Exporter, and Supplier is built on stringent manufacturing standards, advanced technology, and a deep commitment to patient well-being. Pentoxifylline 400mg Tablets – High-Quality Formulation for Improved Peripheral Circulation Pentoxifylline is widely used for conditions associated with peripheral vascular disease and intermittent claudication, where blood flow in the limbs becomes impaired due to narrowed blood vessels. As a peripheral vasodilator, Pentoxifylline functions by reducing blood viscosity, allowing smoother circulation through the arteries and veins, particularly in the hands and feet. At Taj Pharma, our Pentoxifylline 400mg Tablets are manufactured using premium raw materials and strict quality controls to maintain the highest standards of safety, potency, and bioavailability. Why Taj Pharma is the Most Trusted Pentoxifylline 400mg Tablets Manufacturer in India Pentoxifylline Extended-Release 400mg Tablets Unmatched Manufacturing Standards Our WHO-GMP, ISO-certified facilities ensure compliance with […]
Leading Manufacturer and Supplier of Oxycodone Hydrochloride 20mg Tablets in India Taj Pharma India stands as a premier manufacturer, exporter, and supplier of Oxycodone Hydrochloride 20mg Tablets, headquartered in Vapi, Gujarat. Renowned for its commitment to quality, purity, and pharmaceutical excellence, Taj Pharma has established itself as a trusted brand in the global pharmaceutical industry, supplying to regions including Africa, the Middle East, LATAM, and across PAN India. High-Quality Oxycodone Hydrochloride 20mg Tablets Oxycodone Hydrochloride 20mg Tablets Oxycodone Hydrochloride 20mg Tablets are high-strength prescription opioids specifically designed for managing severe and chronic pain in patients who are opioid-tolerant. These tablets are available in extended-release oral formulations, providing continuous, around-the-clock pain relief over an extended period. At Taj Pharma, we prioritize strict adherence to Good Manufacturing Practices (GMP) and international quality standards, ensuring that each batch of Oxycodone Tablets maintains high purity, consistency, and potency. This commitment to excellence makes us one of the most reliable Oxycodone tablets manufacturers and suppliers in India. Therapeutic Uses of Oxycodone Hydrochloride 20mg Tablets Oxycodone Tablets are prescribed for patients who require long-term opioid therapy when other pain management medications fail or are not well tolerated. The tablets belong to the opioid analgesic class and […]
Leading Manufacturer & Exporter of Oxycodone Hydrochloride 30mg Tablets in India As a globally recognized pharmaceutical organization, Taj Pharma India stands at the forefront as one of the most trusted manufacturers, exporters, and suppliers of Oxycodone Hydrochloride 30mg Tablets. With a world-class manufacturing base in Vapi, Gujarat, and distribution channels extending across India, Africa, the Middle East, LATAM, and global regulated markets, we deliver premium-quality Oxycodone formulations that meet strict international quality and compliance standards. Our commitment is centered on purity, efficacy, and reliability, making Taj Pharma a preferred choice for hospitals, government institutions, pharmacies, and pharmaceutical distributors worldwide seeking finished Oxycodone tablets from a certified and dependable source. What Makes Taj Pharma the Leading Oxycodone Hydrochloride 30mg Tablets Manufacturer? Oxycodone Hydrochloride 30mg Tablets High-Quality Pharmaceutical Formulations Our Oxycodone Hydrochloride 30mg Tablets are manufactured using validated processes and stringent quality protocols. Each tablet is formulated for consistency, ensuring optimum therapeutic performance. Key Advantages: High purity active pharmaceutical ingredient (API) Strict GMP, WHO-GMP & ISO-certified facilities Batch-to-batch consistency Regulatory support documents for exports The product is engineered as a controlled-release oral formulation designed for healthcare use by prescription-only channels. Global Supplier of Oxycodone Hydrochloride 30mg Tablets We are renowned as a […]
Leading Manufacturer & Exporter of High-Quality Levetiracetam Tablets 750mg (Leepra XR) Taj Pharma India stands as a globally trusted and reputed manufacturer, exporter, and supplier of Levetiracetam Tablets 750mg (Leepra XR), offering unmatched purity, precision, and compliance with international manufacturing standards. With a strong manufacturing base in Vapi, Gujarat, we provide world-class formulations for epilepsy management across India, Africa, the Middle East, and Latin America (LATAM). As one of India’s most recognized pharmaceutical companies, we take pride in producing high-quality Levetiracetam Tablets that meet stringent pharmacopeial specifications, ensuring therapeutic consistency and patient safety. About Levetiracetam Tablets 750mg (Leepra XR) Levetiracetam tablets 750mg Levetiracetam, a widely prescribed antiepileptic drug (AED), is used for the treatment of: Epilepsy Partial-onset seizures Generalized tonic–clonic seizures Myoclonic seizures It works by binding to the SV2A (synaptic vesicle protein 2A) receptor sites in the brain, helping stabilize abnormal electrical activity and prevent seizure propagation. Why Taj Pharma India Leads the Market in Levetiracetam Tablets Manufacturing 1. State-of-the-Art Manufacturing Facility in Vapi, Gujarat Our advanced WHO-GMP-approved plants are equipped with cutting-edge technology, automated systems, and stringent quality management to ensure absolute purity and consistent potency in every batch of Levetiracetam Tablets. 2. Expertise in Extended-Release (XR) Formulation […]
Leading Manufacturer and Supplier of Oxycodone Hydrochloride 40mg Tablets in India Taj Pharma India is a renowned and trusted manufacturer, exporter, and supplier of Oxycodone Hydrochloride 40mg Tablets, based in Vapi, Gujarat, India. With an unwavering commitment to quality, purity, and compliance, Taj Pharma has established itself as a premium supplier of high-strength opioid medications catering to markets across India, Africa, the Middle East, and Latin America (LTAM). Oxycodone Hydrochloride 40mg Tablets, a controlled-release opioid analgesic, are prescribed for severe, chronic pain management in patients who require continuous, around-the-clock pain relief and have tolerance to opioid treatments. Taj Pharma ensures that each batch of Oxycodone tablets is manufactured under stringent GMP standards, offering healthcare providers and patients the highest level of efficacy and safety. High-Quality Oxycodone Hydrochloride 40mg Tablets by Taj Pharma Oxycodone Hydrochloride 40mg Tablets At Taj Pharma, we specialize in producing Oxycodone Hydrochloride 40mg Tablets that provide consistent pain relief for patients suffering from moderate to severe pain. Our formulation is designed for controlled-release, ensuring that pain relief is sustained over an extended period, making it ideal for chronic pain management. Each tablet is formulated using pharmaceutical-grade excipients to maintain stability, potency, and bioavailability, guaranteeing that patients receive […]
Leading Manufacturer & Global Supplier of Oxycodone Hydrochloride 80mg Tablets from India As a globally trusted pharmaceutical manufacturer, Taj Pharma India has established a strong position in the regulated and semi-regulated markets for Oxycodone Hydrochloride 80mg Tablets, ensuring unmatched quality, purity, and compliance. With world-class manufacturing facilities in Vapi, Gujarat, we specialize in producing finished dosage formulations of Oxycodone Tablets that meet stringent international regulatory standards. Our advanced production capabilities enable us to serve healthcare distributors, institutional buyers, government procurement agencies, and pharmaceutical importers across India, Africa, the Middle East, LATAM, and CIS regions. Why Taj Pharma is a Trusted Manufacturer of Oxycodone Hydrochloride 80mg Tablets Oxycodone Hydrochloride 80mg Tablets The global demand for high-grade opioid analgesics requires manufacturers who prioritize quality control, regulatory compliance, and responsible pharmaceutical handling. At Taj Pharma, every batch of Oxycodone Hydrochloride 80mg Tablets is manufactured in accordance with: WHO-GMP guidelines ISO-certified quality management systems Stringent analytical quality testing (HPLC, GC, dissolution profiles) Good Distribution Practices (GDP) Our commitment to excellence has earned us recognition as a leading PAN-India and international supplier of Oxycodone formulations. Oxycodone Hydrochloride 80mg Tablets – High-Strength Controlled-Release Formulation Oxycodone Hydrochloride 80mg is a controlled-release opioid analgesic, designed for around-the-clock management […]
Taj Pharma India, one of the world’s leading WHO-GMP, ISO 9001:2018, PIC/S, and EU-GMP–compliant pharmaceutical manufacturers, is proud to expand its collaborative initiatives with Lao People’s Democratic Republic (Lao PDR). With a strong legacy of quality-driven manufacturing, regulatory excellence, and global supply chain capability, Taj Pharma aims to support national healthcare priorities, essential medicine procurement, registration projects, and Ministry of Health (MOH) tenders across Lao PDR. Healthcare Landscape in Lao PDR Lao PDR is committed to universal health coverage and sustainable healthcare growth. However, the country continues to face public health challenges, including: Malaria and Dengue Fever Tuberculosis (TB) HIV/AIDS Respiratory and Gastrointestinal Infections Non-communicable diseases (NCDs) such as diabetes, hypertension, cardiac disorders Maternal and Child Health concerns Nutritional deficiencies & anemia Skin and topical infections prevalent in tropical regions Taj Pharma’s extensive product portfolio aligns strongly with these therapeutic needs. Taj Pharma Essential Medicines Available for Lao PDR Taj Pharma manufactures a wide spectrum of affordable, high-quality essential medicines suitable for public health programs and national tenders in Lao PDR: Anti-Infectives & Anti-Malarials Artemisinin-based combinations Mefloquine Tablets 250 mg Metronidazole formulations Ciprofloxacin, Azithromycin, Ceftriaxone, Amoxicillin Rilmenidine Dihydrogen Phosphate Tablets 1mg Anti-Tuberculosis Medicines Rifampicin Isoniazid-based combinations Ethambutol Pyrazinamide HIV / […]
Leading Manufacturer & Exporter of High-Quality Liothyronine Tablets in India Taj Pharma India stands as one of the most trusted and well-recognized manufacturers, suppliers, and exporters of Liothyronine Tablets across India, Africa, the Middle East, LATAM, and global regulated markets. With a strong pharmaceutical legacy and state-of-the-art facilities in Vapi, Gujarat, we ensure the production of premium-grade Liothyronine Sodium Tablets 20mcg, known for purity, efficacy, and consistent therapeutic performance. Liothyronine is a crucial medication used worldwide for the treatment of hypothyroidism (underactive thyroid), helping restore normal hormone levels, energy balance, and metabolic functions. As a leading Liothyronine Tablets manufacturer in India, Taj Pharma maintains the highest quality benchmarks aligned with international regulatory standards. Liothyronine 20mcg Tablets High-Quality Liothyronine Tablets Manufacturer in India We specialize in the production of Liothyronine Sodium Tablets 20mcg, formulated with precision to ensure optimal therapeutic outcomes. Each batch is manufactured in EU-GMP, WHO-GMP, and ISO-certified facilities, offering unmatched quality, safety, and purity. Liothyronine Sodium (T3) is a synthetic version of the natural thyroid hormone triiodothyronine, prescribed to replace deficient hormone levels in patients with hypothyroidism. Our formulations are designed to deliver consistent absorption, predictable action, and reliable improvement of thyroid performance. Why Taj Pharma India Leads […]
Leading Manufacturer & Exporter of High-Quality Levetiracetam Tablets 1000mg (Leepra XR) As a globally trusted pharmaceutical manufacturer, we at Taj Pharma India take immense pride in offering premium-quality Levetiracetam Tablets 1000mg (Leepra XR), engineered with precision, purity, and advanced formulation standards. With a strong presence across India, Africa, the Middle East, LTAM, and several regulated and semi-regulated markets, we continue to lead as one of the most reputable Levetiracetam Tablets Manufacturers & Exporters in the industry. Our manufacturing base in Vapi, Gujarat, is supported by state-of-the-art technology, stringent quality control systems, and world-class R&D facilities. This ensures delivery of safe, reliable, and effective Levetiracetam Tablets designed for consistent therapeutic performance. What Are Levetiracetam Tablets 1000mg (Leepra XR)? Levetiracetam Tablets 1000mg Levetiracetam 1000mg (Leepra XR) is a widely prescribed antiepileptic medication used for the management and control of: Epilepsy Seizure disorders Partial-onset seizures Generalized tonic-clonic seizures Myoclonic seizures The active ingredient, Levetiracetam, binds to specific receptors (SV2A) in the brain, helping stabilize electrical activity and reduce seizure frequency. Why Taj Pharma India Leads in Levetiracetam Manufacturing 1. WHO-GMP, ISO & Global Quality Standards Levetiracetam tablets (Leepra) Our facilities comply with WHO-GMP, ISO-certified systems, and advanced FDA-standard quality controls, ensuring: Absolute drug […]
Leading Manufacturer & Exporter of Theophylline Prolonged-Release Tablets 200mg Taj Pharma India stands as a trusted and globally recognized manufacturer, exporter, and supplier of Theophylline Prolonged-Release Tablets 200mg, delivering uncompromised quality, safety, and efficacy. With a world-class manufacturing unit located in Vapi, Gujarat, we uphold international standards to supply premium-grade bronchodilator formulations across India, Africa, the Middle East, Latin America (LTAM), and other global markets. Our Theophylline Prolonged-Release Tablets 200mg are formulated to ensure controlled and sustained release, offering consistent therapeutic benefits for patients suffering from asthma and chronic obstructive pulmonary disease (COPD). Known for reliability, purity, and precision, Taj Pharma continues to be the preferred choice for global pharmaceutical distributors, importers, hospitals, and PCD franchise partners. Theophylline Prolonged-Release Tablets 200mg Why Taj Pharma is the Leading Manufacturer of Theophylline Prolonged-Release Tablets 200mg As a reputed pharmaceutical producer, we ensure: High-purity APIs WHO-GMP and ISO-certified facilities Strict quality control checks Regulatory compliance for exports Controlled-release technology for optimal drug delivery Our customers rely on us because we deliver consistent quality, prompt supply, and industry-leading manufacturing standards. Understanding Theophylline Prolonged-Release Tablets 200mg Theophylline Prolonged-Release Tablets Theophylline is a well-established bronchodilator that assists in relaxing airway smooth muscles, improving airflow, and restoring […]
Taj Pharma India, a globally recognized pharmaceutical manufacturer with WHO-GMP, ISO 9001:2018, GMP/GLP, PIC/S–aligned facilities, is expanding its commitment to supporting the healthcare infrastructure of Thailand. With a strong regulatory foundation, advanced manufacturing capabilities, and a comprehensive essential medicine portfolio, Taj Pharma aims to contribute significantly to Thailand’s public health programs, government tenders, and Ministry of Public Health (MOPH) procurement initiatives. Healthcare Landscape in Thailand Thailand has one of Southeast Asia’s most advanced public health systems, supported by successful universal health coverage (UHC). However, the country faces persistent medical challenges, including: Communicable Diseases Dengue Fever Tuberculosis (TB) HIV/AIDS Influenza Respiratory infections Non-Communicable Diseases Diabetes Hypertension Cardiovascular disease Cancer Chronic kidney disease Public Health Challenges Ageing population Maternal and child health needs Antimicrobial resistance (AMR) Urban lifestyle-related disorders Taj Pharma’s product range meets these needs with internationally compliant, affordable pharmaceutical solutions. Taj Pharma Medicines for Thailand’s Major Health Needs 1. Anti-Infectives & Antibiotics Azithromycin, Amoxicillin-Clavulanic Acid Ceftriaxone, Cefixime, Levofloxacin Metronidazole, Ciprofloxacin 2. Anti-Malarial & Anti-Dengue Supportive Medicines Mefloquine Tablets 250 mg Paracetamol, ORS, IV Fluids Pain management & supportive therapy 3. Tuberculosis (TB) Treatment Portfolio Isoniazid Rifampicin Pyrazinamide Ethambutol Fixed-dose combinations 4. HIV/Antiretroviral Therapy (ART) Medicines Tenofovir Lamivudine Efavirenz Dolutegravir-based regimens […]
Leading Manufacturer & Exporter of Tigecycline Injection 50mg (Tygisafe) in India Taj Pharma India stands as a trusted, reputed, and globally recognized manufacturer, exporter, and supplier of Tigecycline Injection 50mg (Tygisafe). With a strong manufacturing base in Vapi, Gujarat, and corporate presence in Mumbai, we deliver pharmaceutical excellence backed by stringent quality standards, international certifications, and robust supply-chain efficiency. Our legacy in producing high-purity, safe, and reliable Tigecycline Injection formulations positions us as the preferred partner across India, Africa, the Middle East, LATAM, CIS countries, and global regulated markets. What is Tigecycline Injection 50mg (Tygisafe)? Tigecycline is a broad-spectrum antibiotic used to treat severe and complicated bacterial infections. It works by inhibiting bacterial protein synthesis, preventing harmful bacteria from growing and multiplying. Taj Pharma manufactures Tygisafe, a high-quality, GMP-certified Tigecycline Injection 50mg that is widely trusted in hospitals, emergency care units, and clinical settings for serious infections. Why Taj Pharma India is the Top Tigecycline Injection Manufacturer in India Tigecycline Injection (TygiSafe) 1. High-Quality Manufacturing in Vapi, Gujarat We produce Tigecycline Injection 50mg (Tygisafe) in ultra-modern, WHO-GMP, ISO-certified facilities ensuring: Absolute purity Enhanced stability Clinical-grade safety Consistent therapeutic efficacy 2. Strict Quality Control & International Compliance Our formulations undergo: Sterility […]
Toremifene Citrate Tablets 60mg (TOREMITAJ) – Leading Manufacturer & Global Supplier Taj Pharma India stands as a trusted, well-established, and globally recognized manufacturer, exporter, and supplier of Toremifene Citrate Tablets 60mg (TOREMITAJ). As one of India’s most respected pharma companies based in Vapi, Gujarat, we are committed to delivering premium-grade oncology medicines with uncompromised quality, purity, and regulatory compliance. Our Toremifene Citrate Tablets 60mg are formulated to meet global standards and are exported to Africa, the Middle East, LATAM, CIS, Southeast Asia, and other international markets. As a leading manufacturer in India, we ensure consistency, precision, and therapeutic effectiveness in every batch. Understanding Toremifene Citrate Tablets 60mg (TOREMITAJ) Toremifene Citrate is a selective estrogen receptor modulator (SERM) used primarily for treating metastatic breast cancer in postmenopausal women whose tumors are hormone-receptor positive. Many breast cancer tumors grow in response to estrogen. Toremifene Citrate works by blocking the estrogen hormone, inhibiting tumor growth and aiding in disease management. At Taj Pharma India, we manufacture TOREMITAJ Tablets under stringent quality control, ensuring that each tablet meets international safety and efficacy benchmarks. Why Toremifene Citrate is Important in Breast Cancer Treatment Toremifene Citrate Tablets 60mg Hormone-receptor Positive Metastatic Breast Cancer Breast cancer that […]
Leading Manufacturer & Exporter of High-Quality Penicillamine Capsules 125mg As a globally trusted pharmaceutical organization, Taj Pharma India stands as a well-known Penicillamine Capsules 125mg manufacturer in India, delivering unmatched purity, quality, and therapeutic excellence. With a strong footprint across India, Africa, the Middle East, and Latin America (LTAM), we are recognized as one of the most reliable and premium suppliers and exporters of Penicillamine Capsules. Our advanced manufacturing facility in Vapi, Gujarat, adheres to the highest international quality benchmarks including WHO-GMP, ISO, and regulatory certifications. This enables us to supply clinically dependable and affordable Penicillamine Capsules to global markets. What Are Penicillamine Capsules 125mg? Penicillamine Capsules 125mg are a well-established medication used in the treatment of several chronic and rare disorders. They work by: Blocking inflammatory chemical messengers responsible for rheumatoid arthritis Slowing the progression of joint-related diseases Binding and removing excess copper from the body in Wilson’s disease Binding cystine and heavy metals, making it useful for conditions such as cystinuria These mechanisms make Penicillamine one of the most important therapeutics in the category of chelating agents and anti-rheumatoid drugs. Why Taj Pharma Is the Top Manufacturer of Penicillamine Capsules 125mg Penicillamine Capsules 125mg Commitment to Quality & […]
Leading Manufacturer & Exporter of Ampicillin for Injection 500mg in India Taj Pharma India stands as a globally trusted manufacturer, exporter, and supplier of Ampicillin for Injection 500mg from Vapi, Gujarat, India. With a reputation built on uncompromised quality, purity, and regulatory excellence, we offer premium-grade Ampicillin Injection solutions for global healthcare markets, including Africa, the Middle East, LATAM, CIS countries, and PAN India. As one of the top Ampicillin Injection manufacturers in India, Taj Pharma adheres to stringent international manufacturing standards, ensuring every vial meets the highest benchmarks for safety, efficacy, and pharmaceutical consistency. Ampicillin for Injection 500mg What is Ampicillin Injection 500mg? Ampicillin Injection is a penicillin-type broad-spectrum antibiotic effective against a wide variety of bacterial infections. It is commonly prescribed for: Ear, nose & throat infections Respiratory tract infections (including pneumonia) Urinary tract infections Gastrointestinal infections Meningitis Bloodstream infections Heart infections Skin & soft tissue infections Administered via intravenous infusion (IV) or intramuscular (IM) route, this medication is always given under medical supervision. Why Taj Pharma India is the Leading Ampicillin Injection Manufacturer At Taj Pharma India, we combine decades of pharmaceutical expertise with cutting-edge manufacturing technology to deliver world-class injectable formulations. Ampicillin for Injection 500mg ✔ […]
Leading Manufacturer & Global Supplier of Urokinase for Injection 5000IU (UVANTAJ) Taj Pharma India stands as one of the most trusted, reputable, and quality-driven manufacturers of Urokinase for Injection 5000IU (UVANTAJ) in India. With a proven commitment to purity, efficacy, and international manufacturing standards, Taj Pharma has earned recognition across India, Africa, the Middle East, LATAM, and CIS regions for delivering premium-grade Urokinase formulations to healthcare providers worldwide. Urokinase for Injection is a life-saving thrombolytic medication used to dissolve harmful blood clots in the arteries and veins. It plays a crucial role in the management of acute myocardial infarction (heart attack), pulmonary embolism, stroke, and deep vein thrombosis (DVT). As a critical-care medicine, its manufacturing demands extreme precision, sterile production units, and stringent quality testing—areas where Taj Pharma India excels beyond expectations. What Makes Taj Pharma India the Most Reliable Manufacturer of Urokinase Injection 5000IU (UVANTAJ)? Urokinase 5000IU Injection State-of-the-Art WHO-GMP & ISO Certified Manufacturing Unit Taj Pharma operates from its advanced manufacturing base in Vapi, Gujarat, equipped with: WHO-GMP certified sterile injectable production lines Dedicated lyophilization facilities High-grade raw material sourcing International quality compliance (IP/BP/USP) Each batch of Urokinase Injection 5000IU undergoes rigorous laboratory testing to ensure purity, stability, […]
Leading Manufacturer and Supplier of Captopril 12.5mg Tablet (CAPOTAJ) Taj Pharma India has established itself as a premier manufacturer, exporter, and supplier of Captopril 12.5mg Tablet (CAPOTAJ), operating from Vapi, Gujarat, India. Renowned for high-quality, pure formulations, Taj Pharma India provides a trusted solution for managing hypertension, heart failure, and the prevention of heart attack and stroke. Our dedication to excellence ensures that patients and healthcare providers worldwide receive the most reliable ACE inhibitor medications. High-Quality Captopril 12.5mg Tablet for Hypertension Management Captopril 12.5mg Tablet Captopril is a well-known angiotensin-converting enzyme (ACE) inhibitor that plays a vital role in reducing blood pressure and enhancing heart efficiency. By relaxing blood vessels and improving blood flow, Captopril ensures the heart pumps blood more effectively. This makes it a cornerstone in hypertension management and the prevention of serious cardiovascular events. Our Captopril 12.5mg Tablet is manufactured under stringent quality control standards, ensuring purity, consistency, and efficacy. Healthcare professionals rely on CAPOTAJ as a trusted choice for patients needing long-term blood pressure regulation. Comprehensive Cardiovascular Benefits Captopril 12.5mg Tablet Captopril offers multiple cardiovascular benefits, including: Lowering high blood pressure and reducing the strain on the heart. Prevention of heart attack and stroke by maintaining […]